About ARVIN PUMP
Deliver reliable pump solutions for severe sulfuric acid and oleum applications through engineering excellence, quality assurance, and long-term service commitment.
1976
Founded
60+
Employees
600+
Projects
10000+
Products Sold
Company Profile
Founded in 1976, ARVIN PUMP has achieved sustained development over nearly five decades. With advanced manufacturing equipment, strong R&D capabilities, and ISO 9001:2015 certification, our products serve customers across China and internationally.
ISO 9001:2015 Certified
Quality management system ensuring consistent product standards across all manufacturing processes.
Delivery Reach
Over 10,000 products deliveried to more than 600 projects
Standards Compliant
Designs meet GB/5656, GB/3216, GB/13007, HG20592/RF and related international standards.
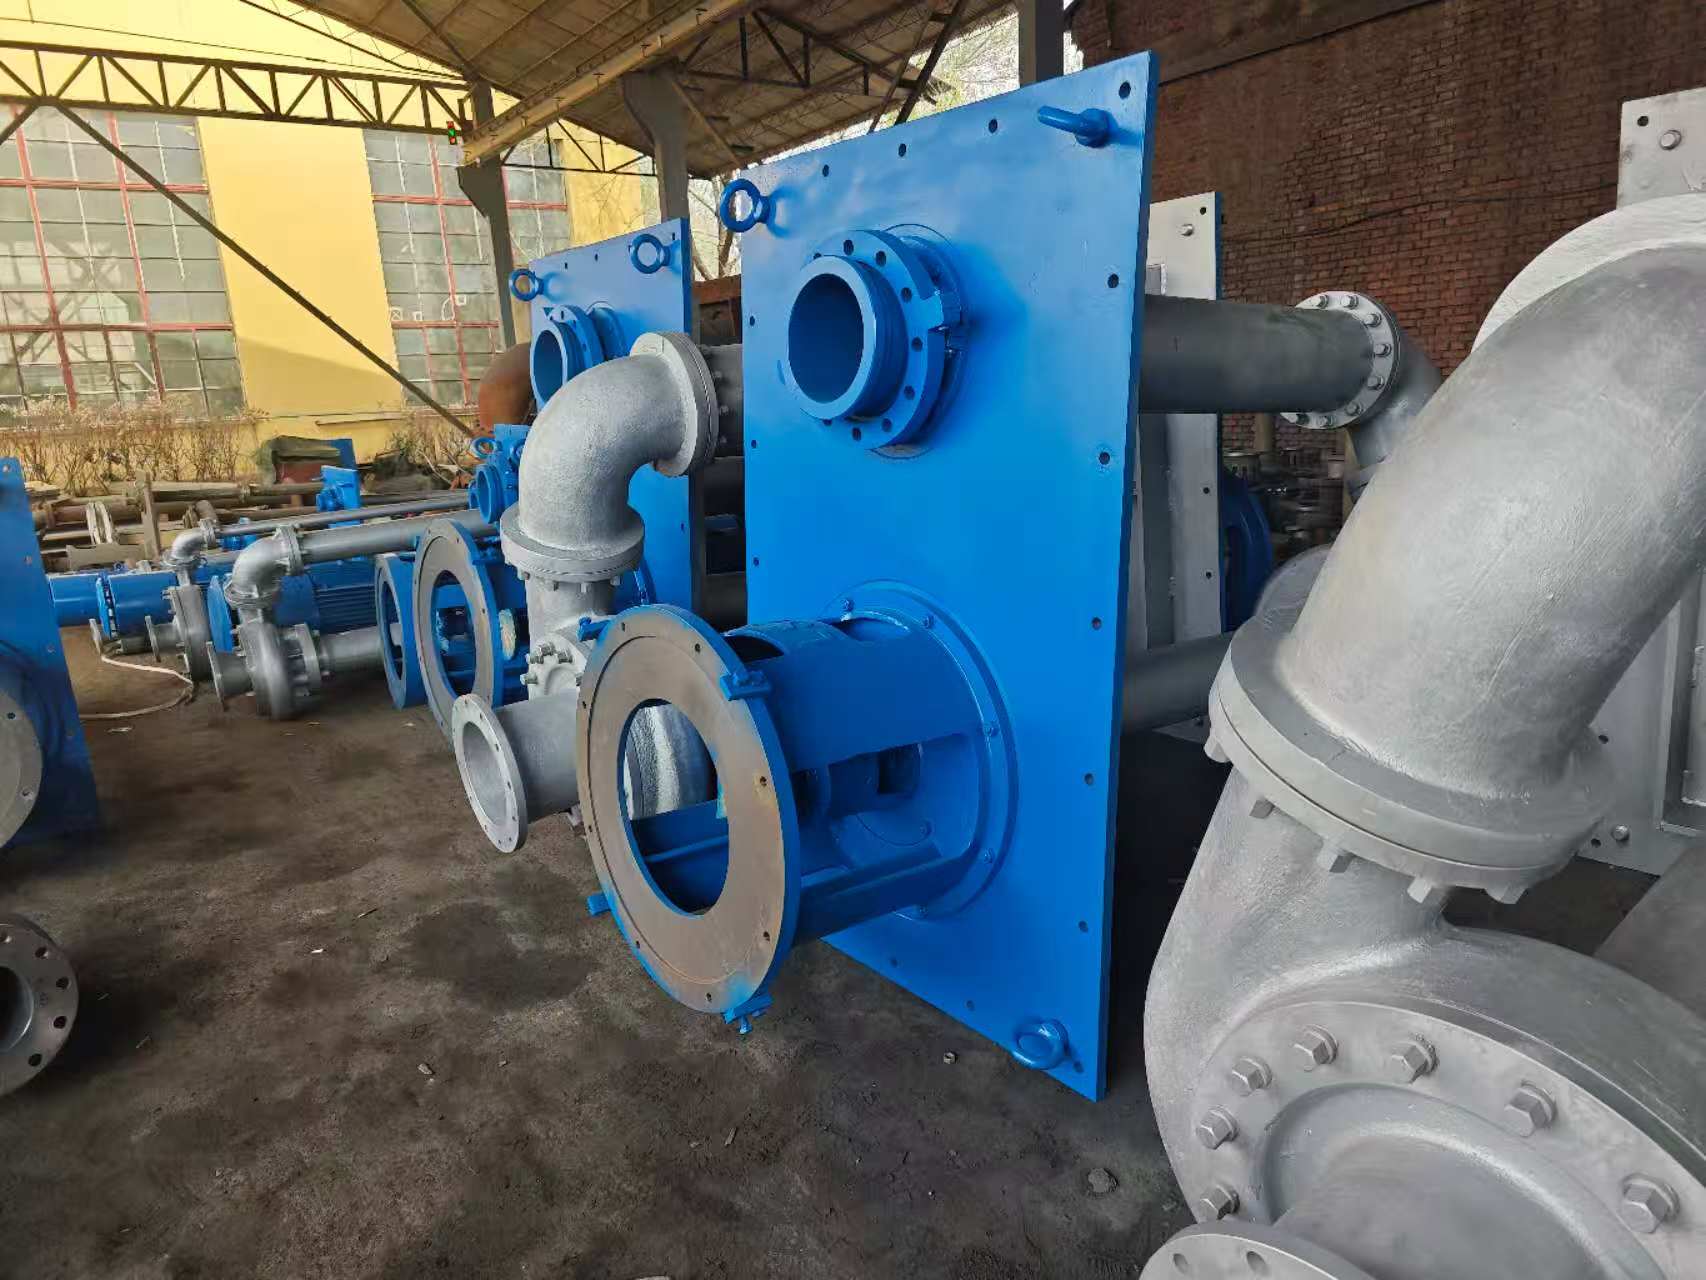
Company History
- 2025
August
- Outstanding Partner on the 30th anniversary of Sulfuric Acid Industry magazine
- 2020
August
- Council member organization, China Sulfuric Acid Industry Association
- 2004
- Advanced enterprise — Lüshunkou District
- 1993
- Second Prize, Chinese Academy of Sciences Science and Technology Progress Award
- First Prize, Liaoning Provincial Spark Program Science and Technology Progress Award
- 1991
- Concentrated sulfuric acid pump — Second Prize, Sun Shibai Sulfuric Acid Technology Development Award Foundation
- High-temperature concentrated sulfuric acid pumps — Silver Award, National Spark Program Achievements Expo (Seventh Five-Year Plan)
- 1976
- Dalian ARVIN PUMP established
Technical Strength
R&D Capability
Continuous development and optimization for high-temperature, high-concentration acid service applications.
Materials & Alloys
Special alloy shafts and wetted parts ensure superior corrosion resistance and long service life.
Manufacturing & QA
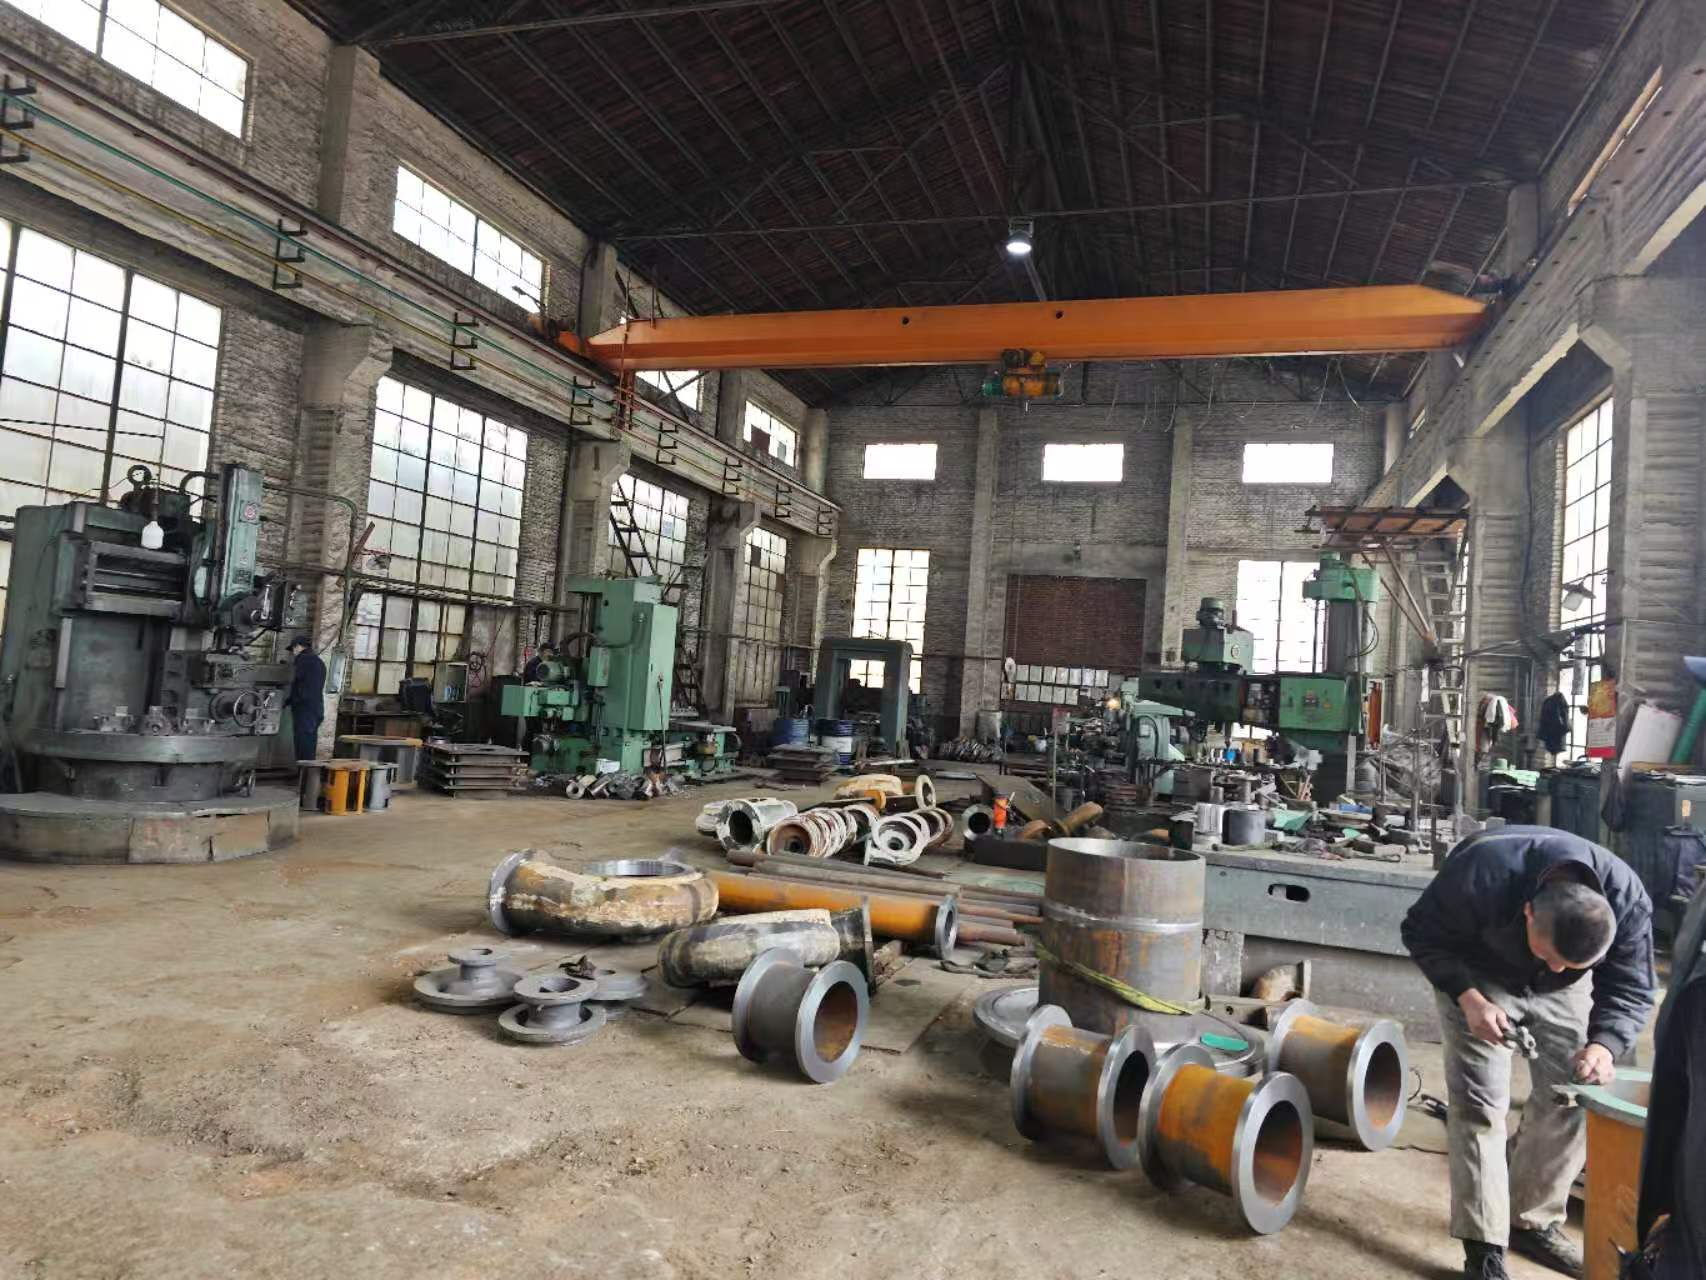
Professional production with dedicated workshops, process control, and ISO 9001:2015 certified quality system.
Built on Partnerships, Delivered with Precision
Technical Capability
To consistently deliver the industry's most reliable equipment and solutions, we have established long-standing R&D partnerships with leading Chinese institutes. Co-developed with the Shanghai Institute of Metallurgy (CAS), our high-temperature concentrated sulfuric acid submersible pump series received a National Science & Technology Progress Award, was named a 1993 National New Product, and is protected by national patents — a strong technical backbone behind every project we deliver.
Long-term R&D partners
Delivery Capability
A mature, efficient operations management model — backed by a robust supplier network and our own integrated manufacturing base — ensures every order is delivered on time and to specification. From raw alloy procurement through machining, assembly and final QA, production stays under one roof so customers receive a single, accountable point of ownership for every pump that leaves the factory.
On-Time
Scheduled Delivery
In-House
Manufacturing Base
100%
QA Inspection
Product Scope
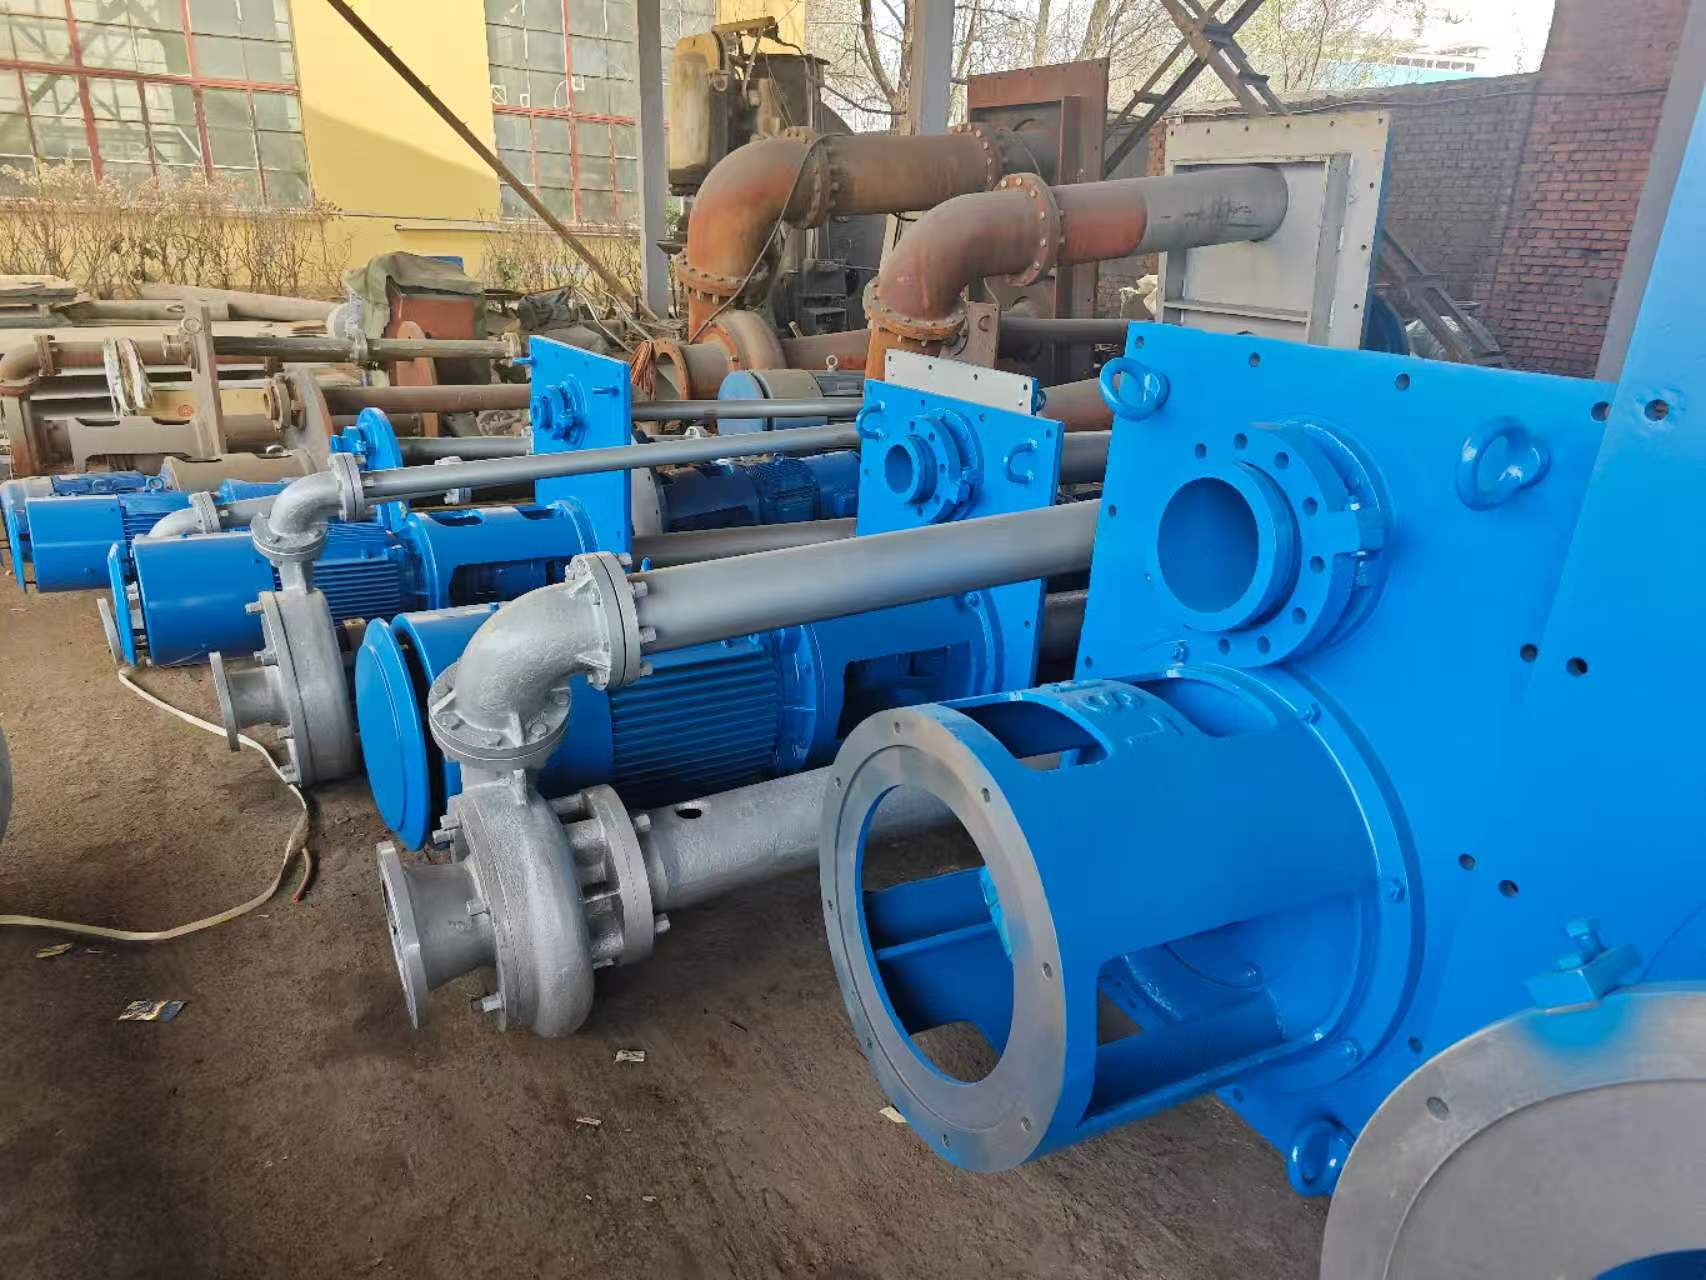
Focused on pump solutions for the sulfuric acid industry — the CSP Series concentrated sulfuric acid submerged pump and the MSB Series molten sulfur pump — engineered for severe high-temperature, corrosive service.
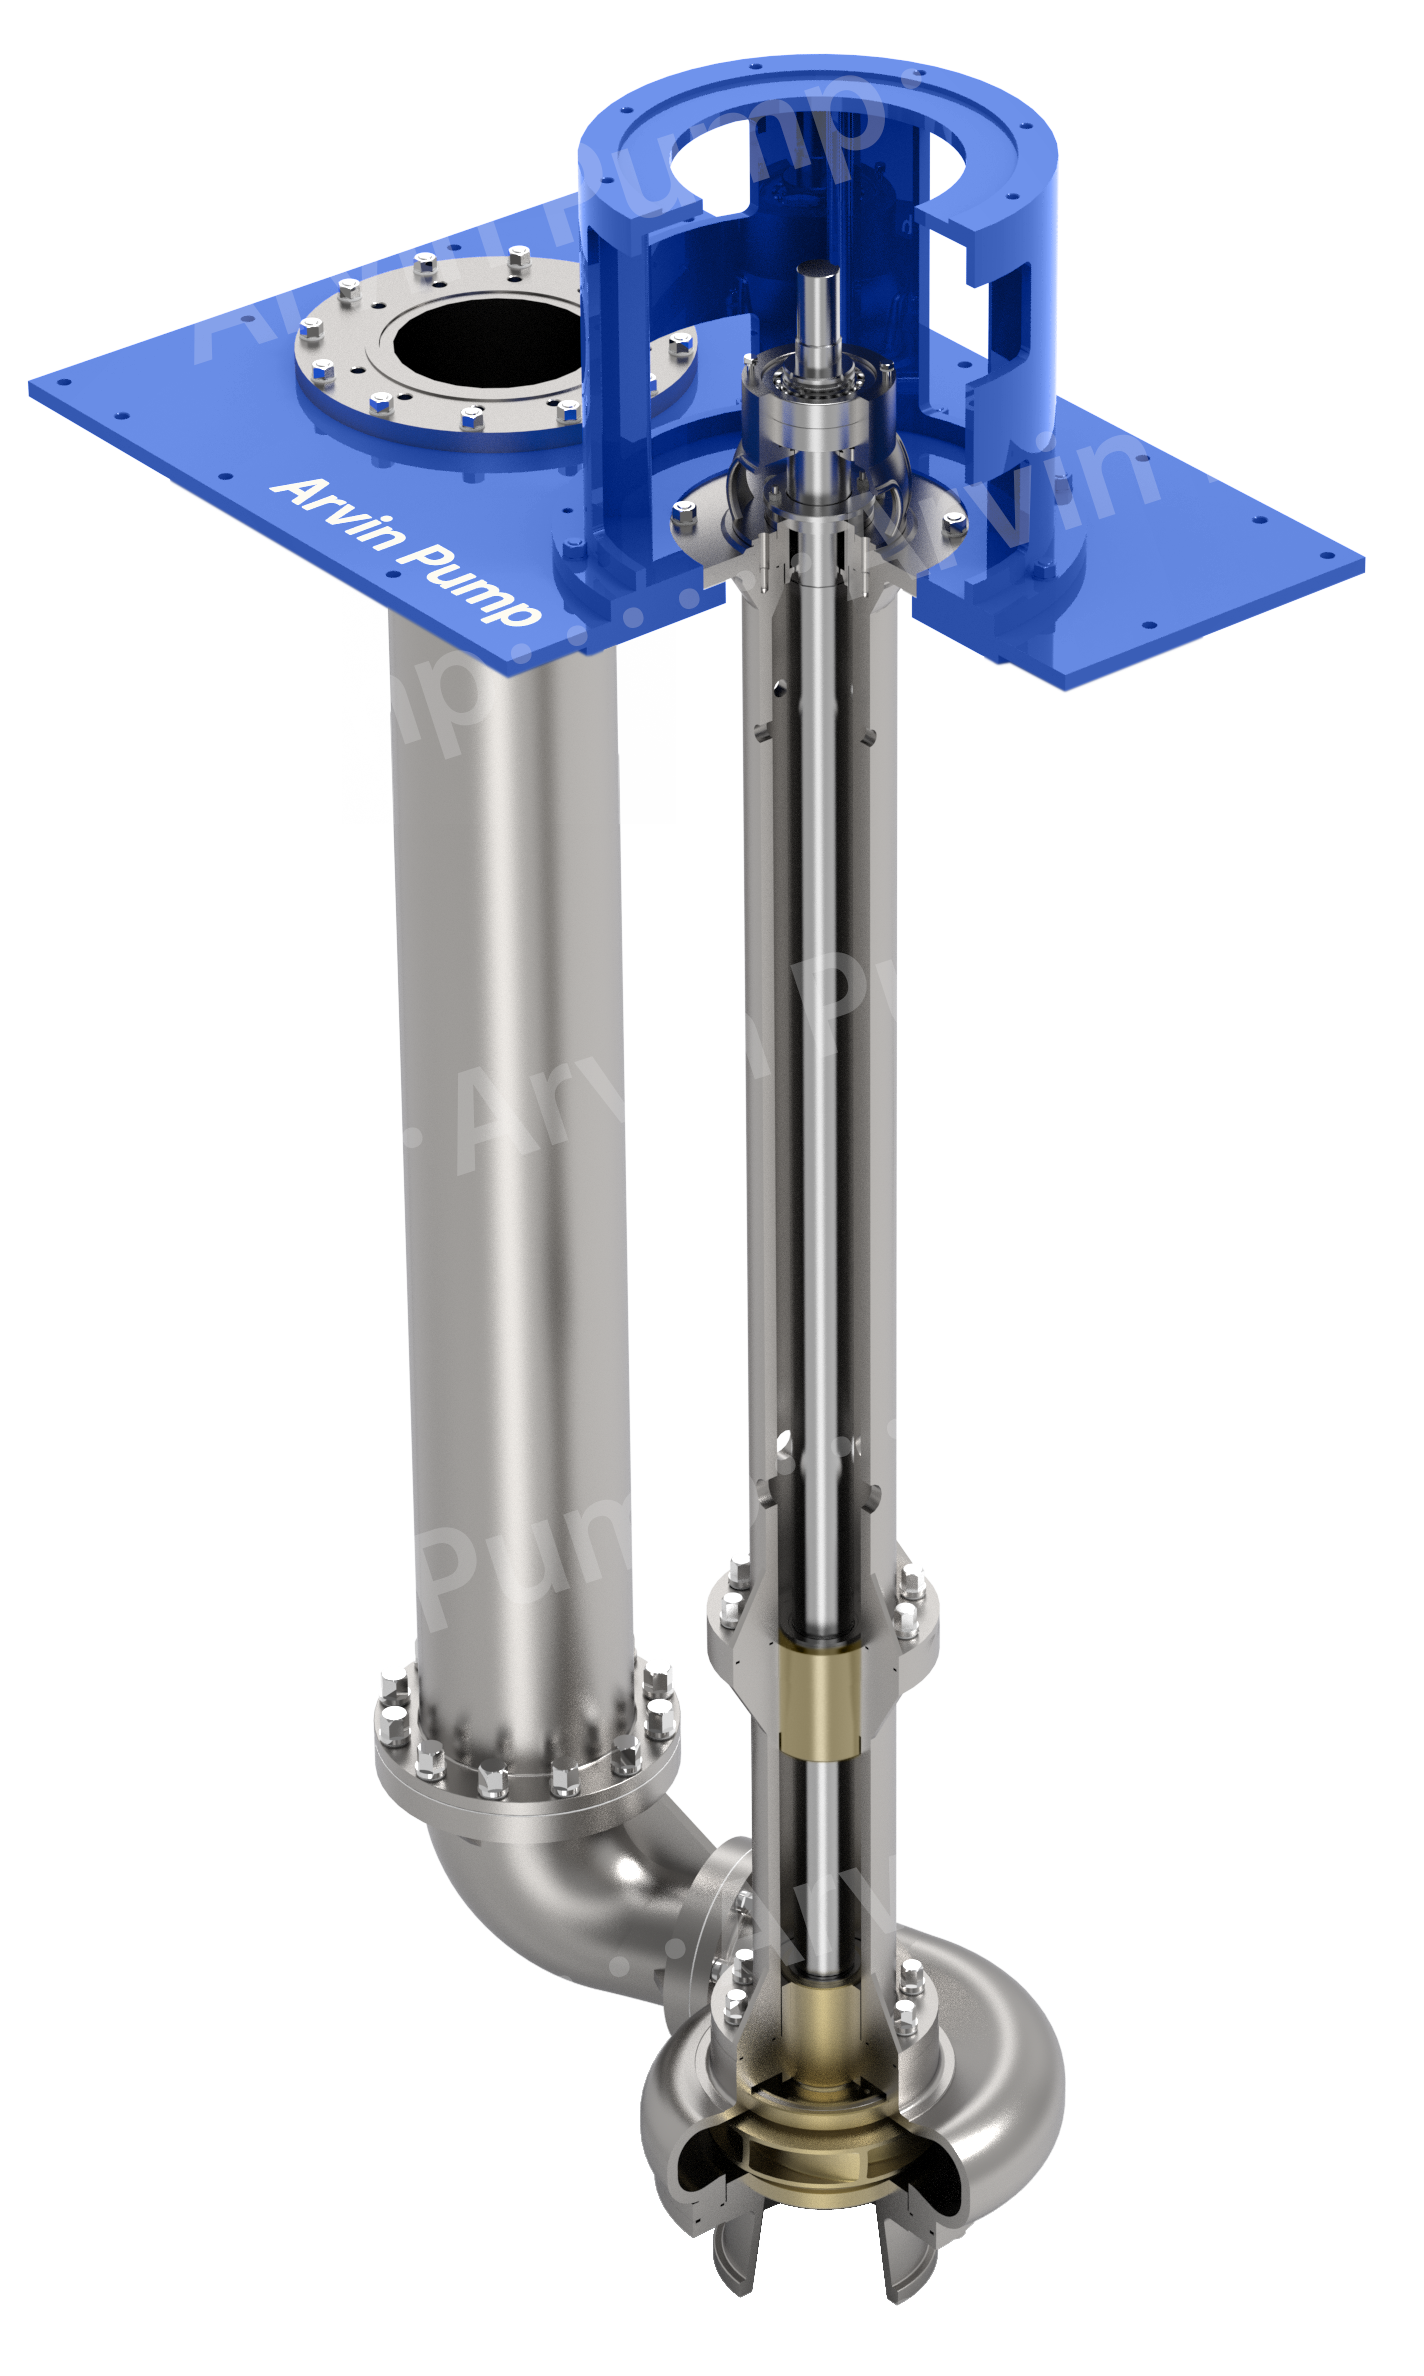
CSP Series
High-Efficiency Intelligent High-Temperature Concentrated Sulfuric Acid Submerged Pump
~2400
m³/h
Capability
~60
m
Head
250
℃
Max Temp
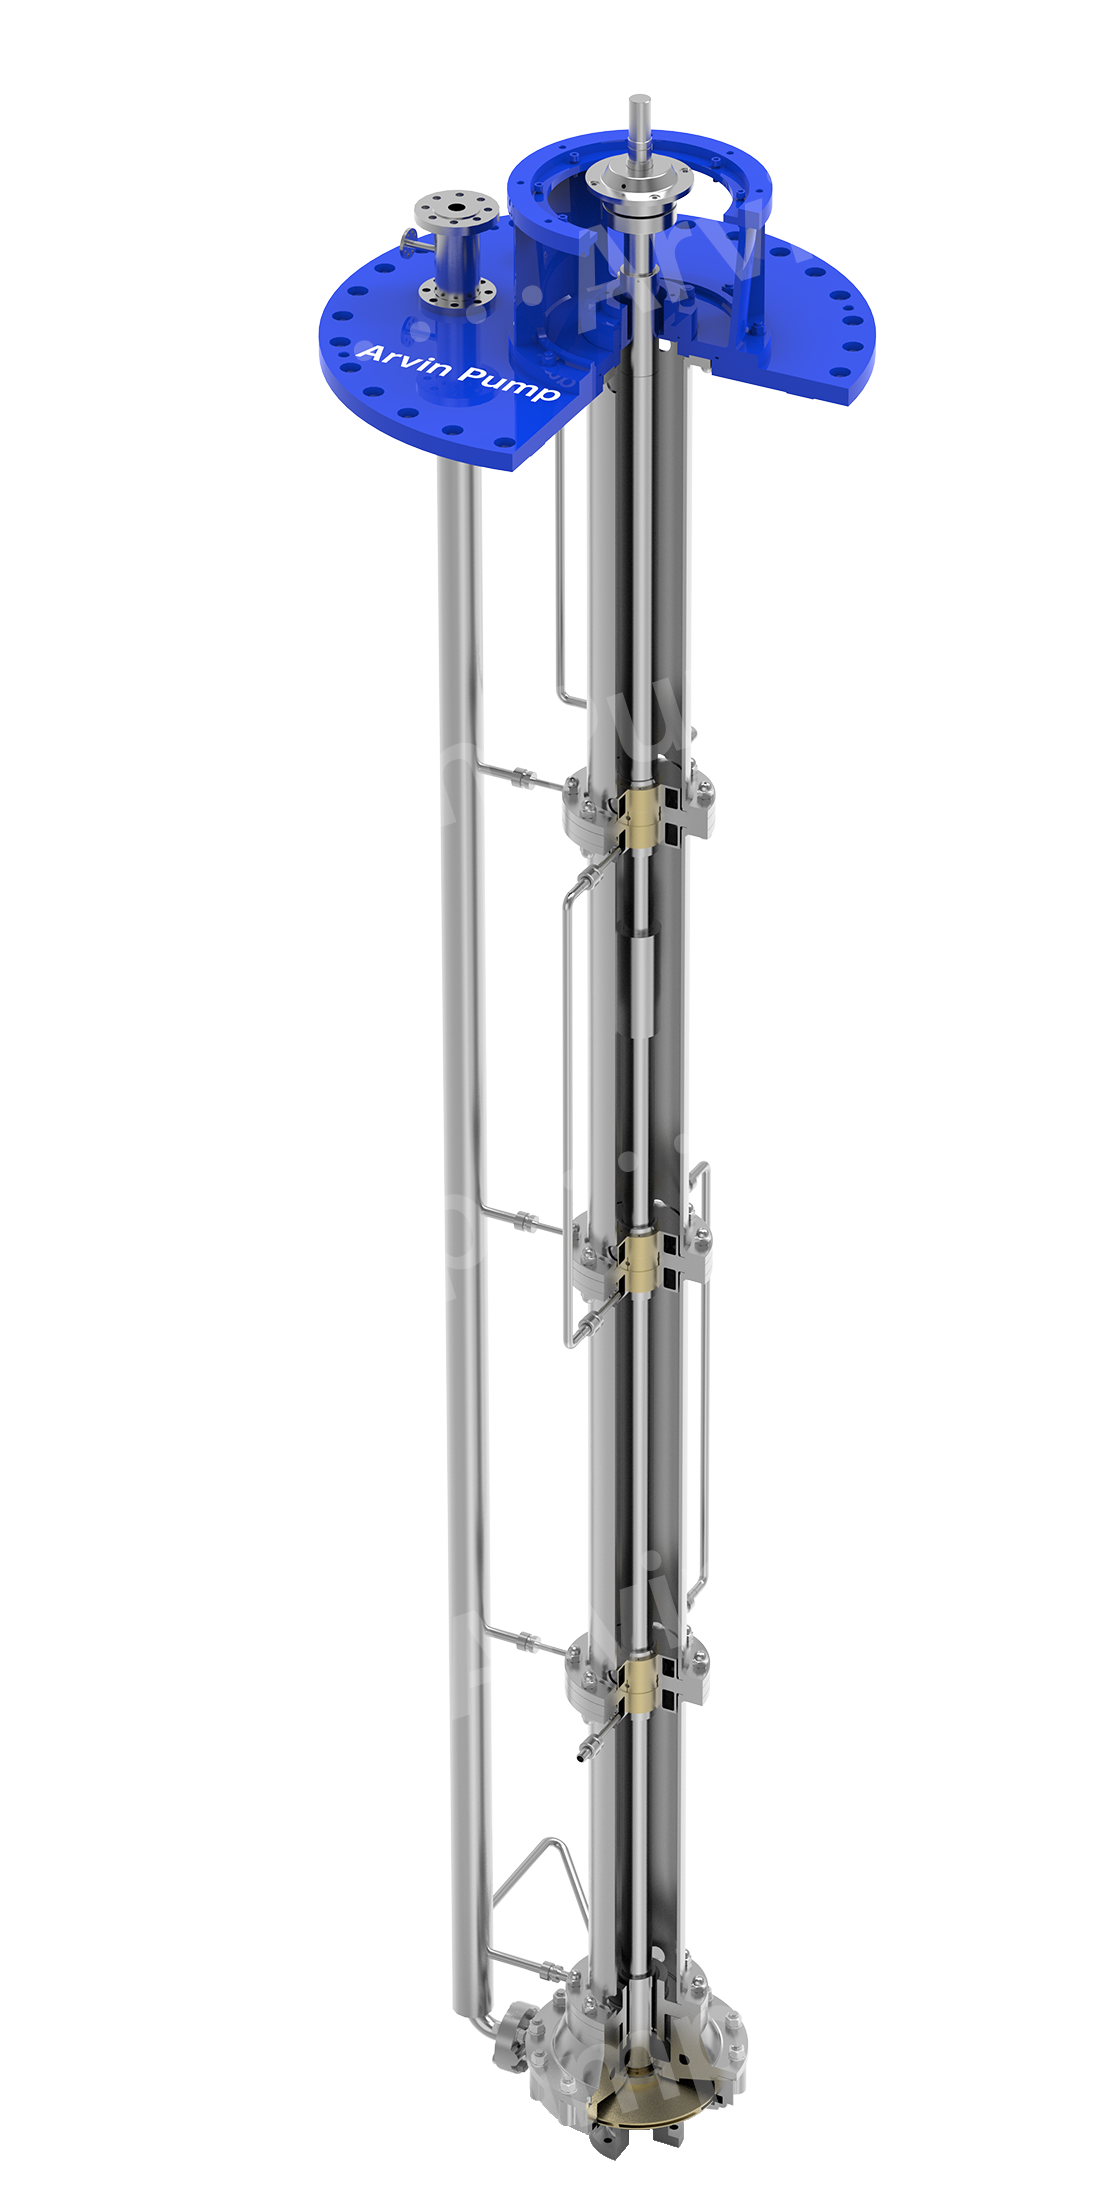
MSB Series
High-Efficiency Molten Sulfur Pump
~150
m³/h
Capability
~150
m
Head
180
℃
Max Temp
Workshop Photos
Manufacturing workshop 1
Manufacturing workshop 2
Manufacturing workshop 3
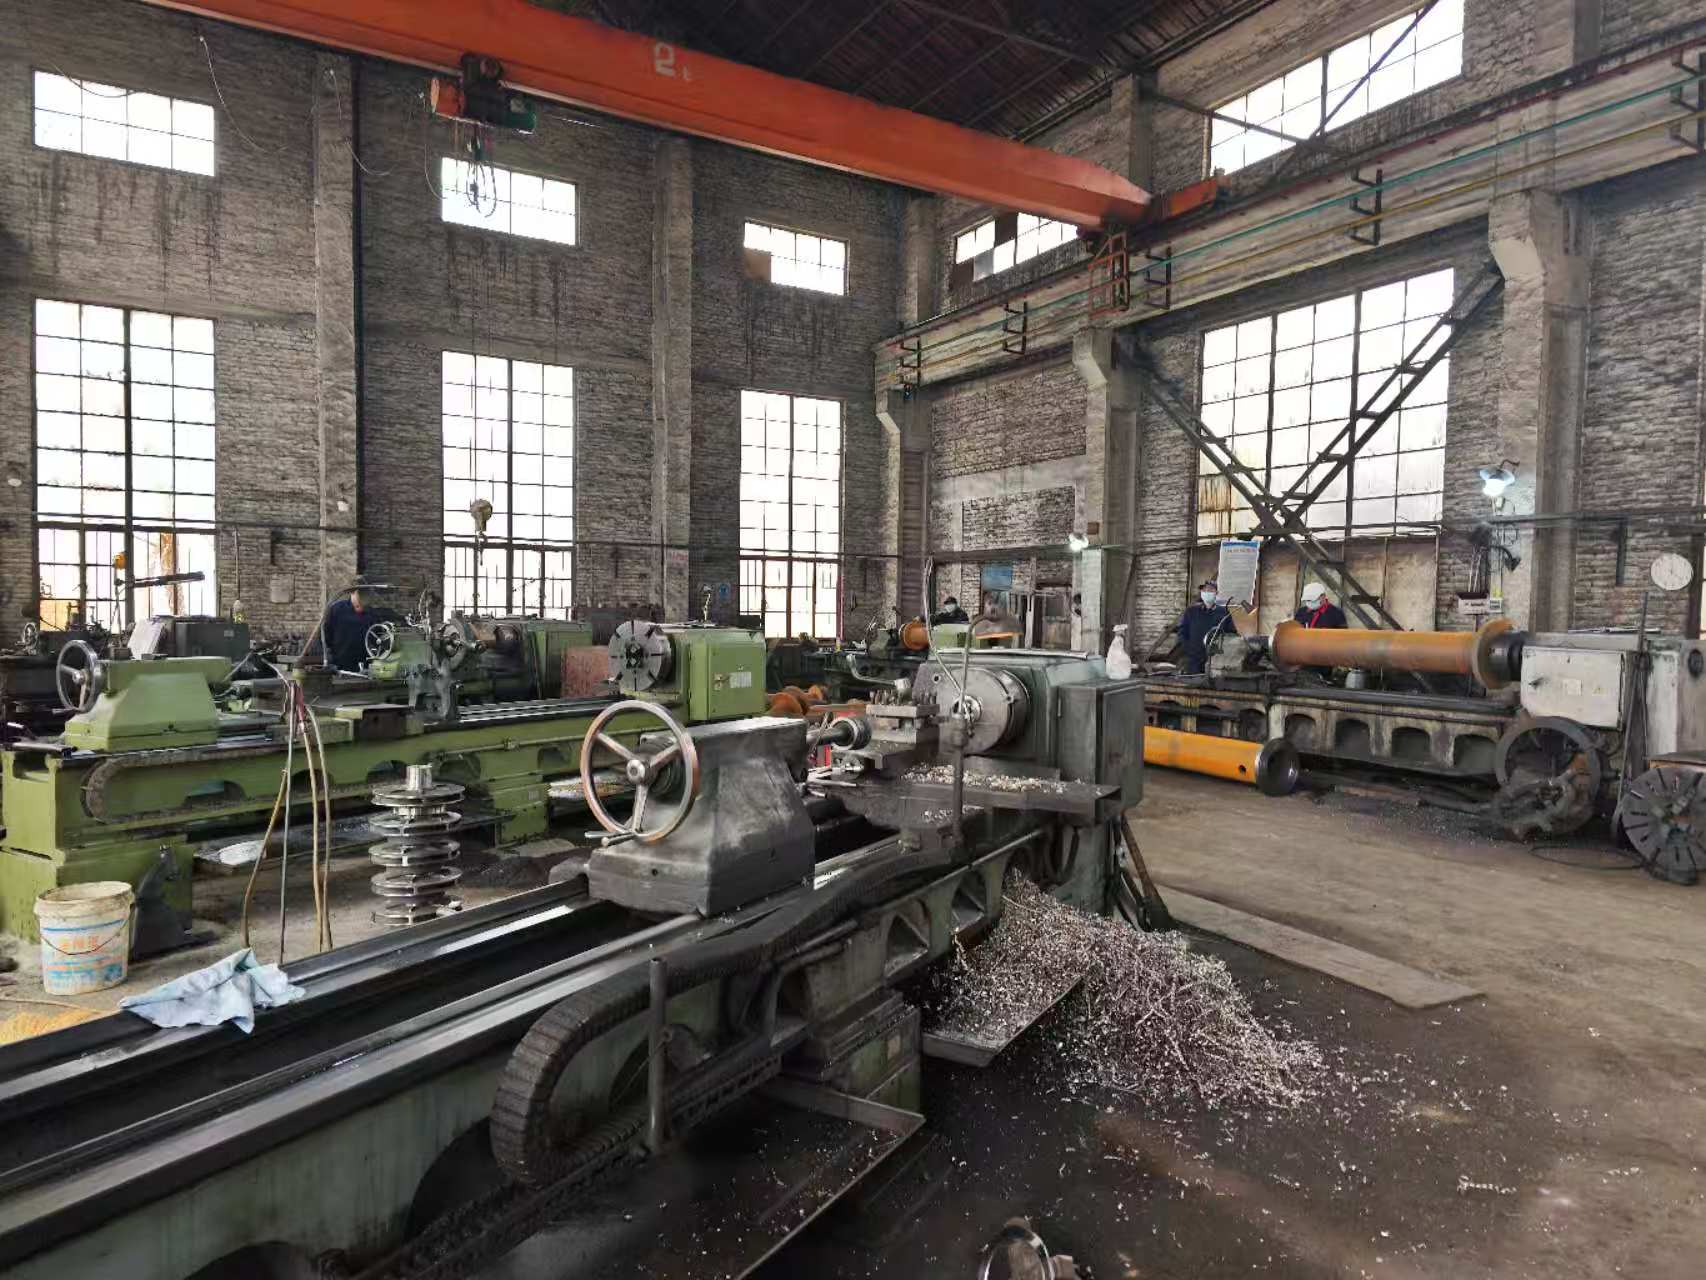
Manufacturing workshop 4
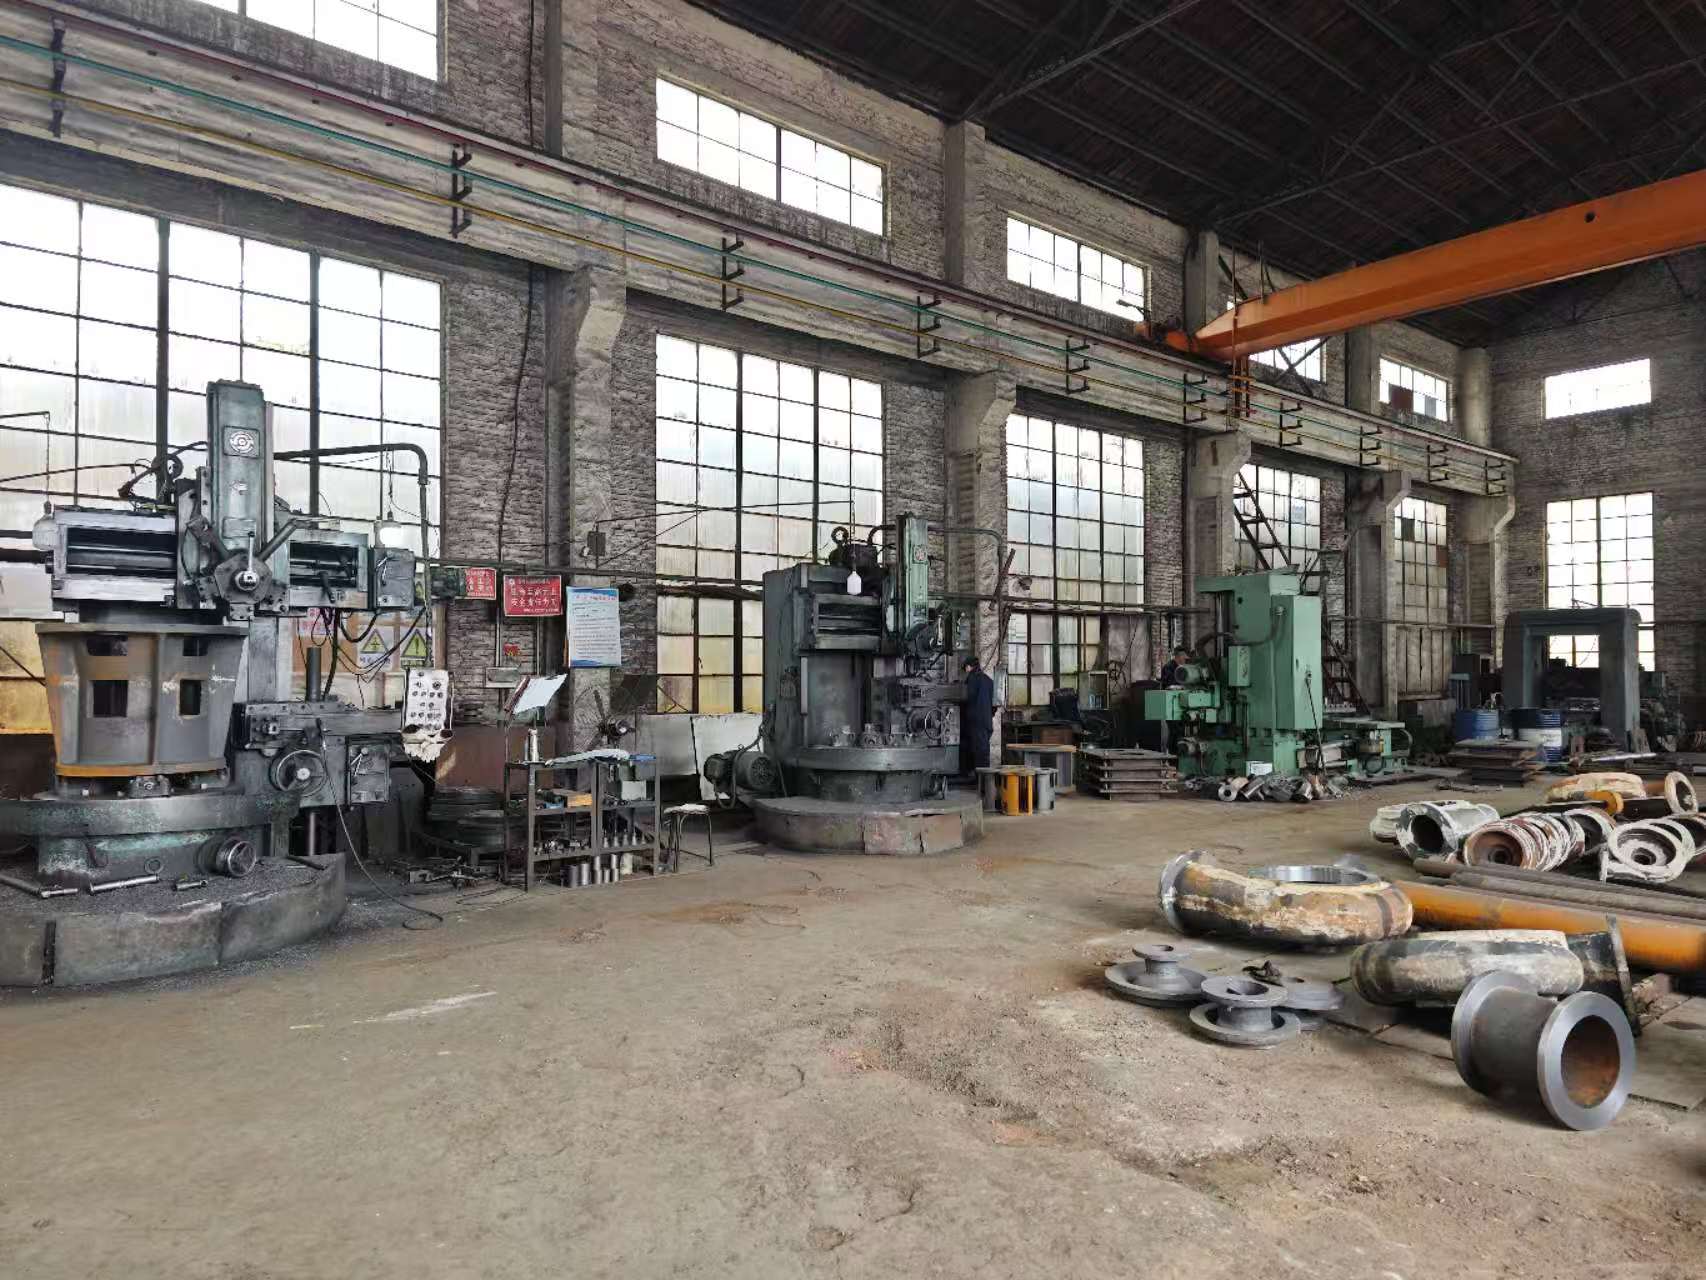
Manufacturing workshop 5
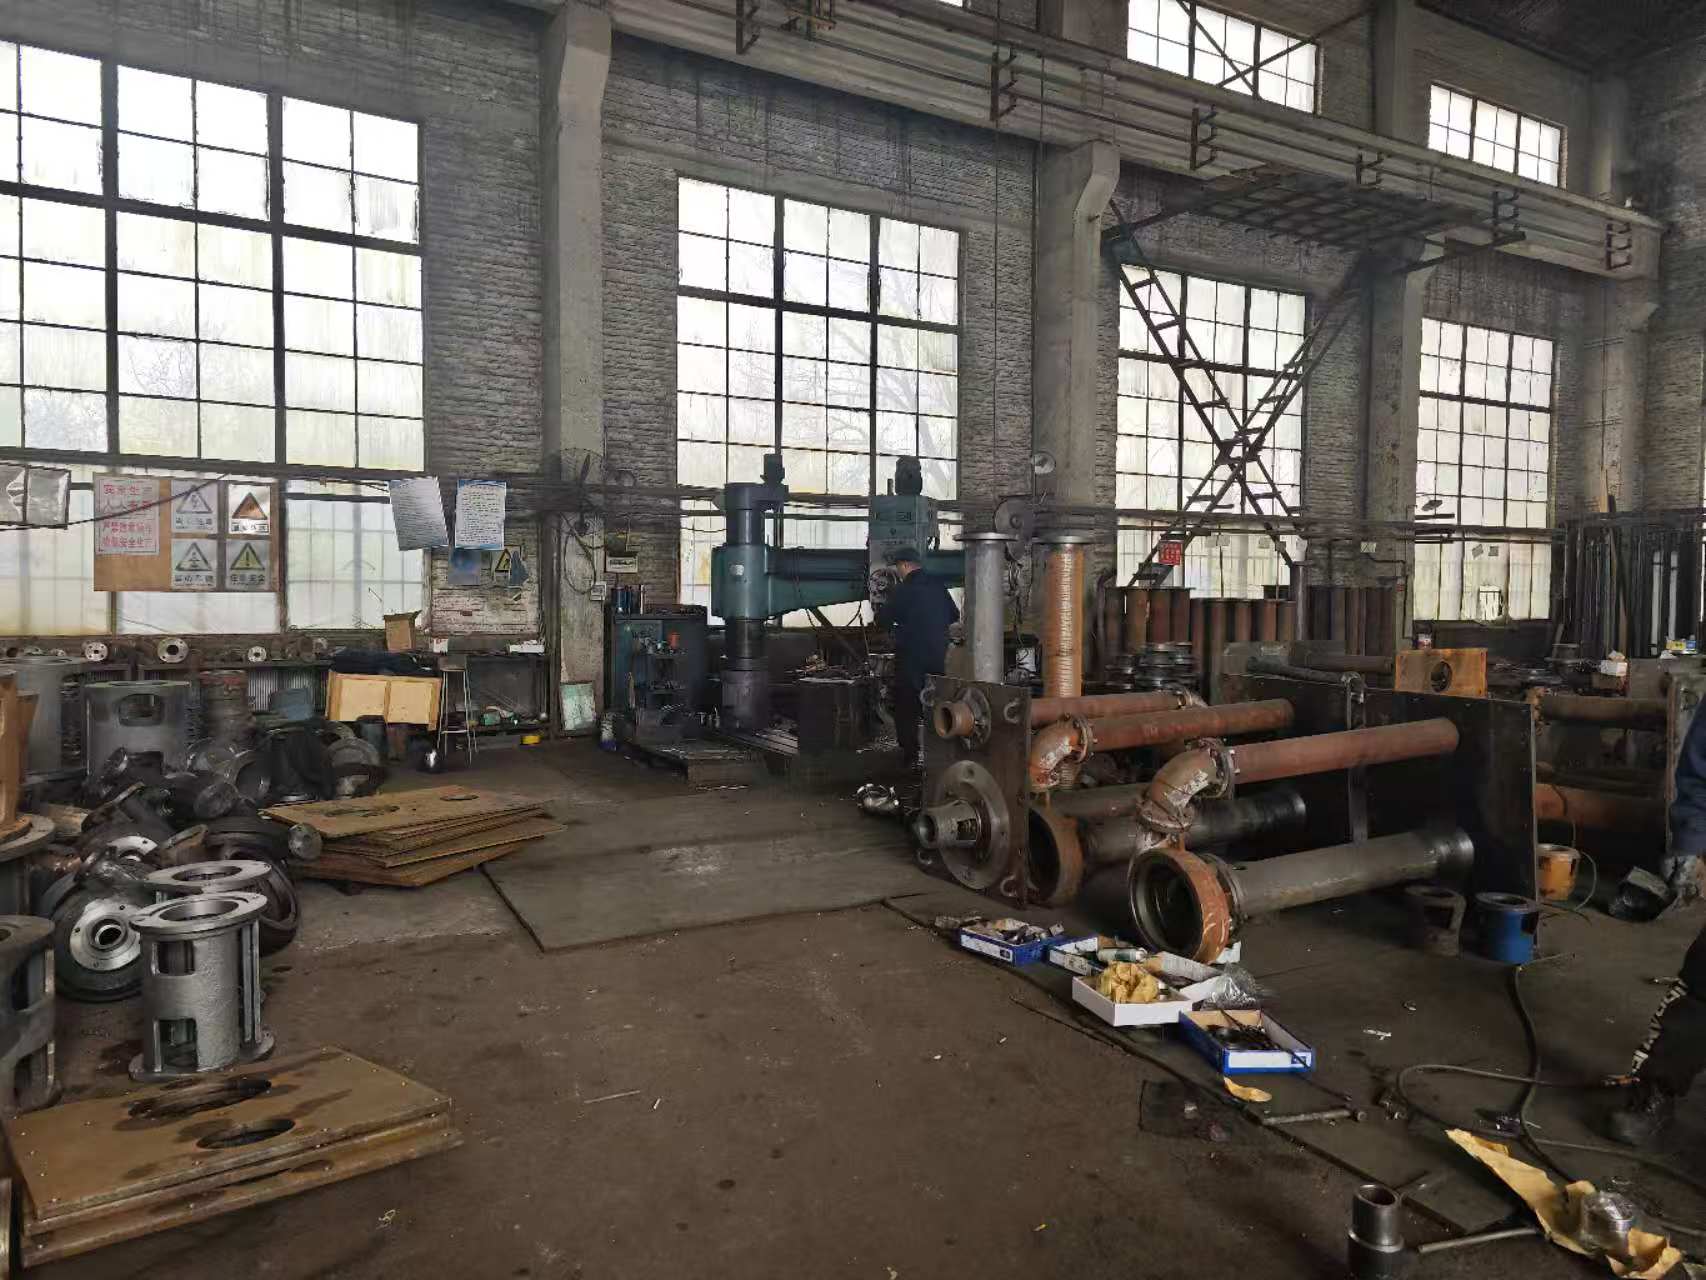
Manufacturing workshop 6
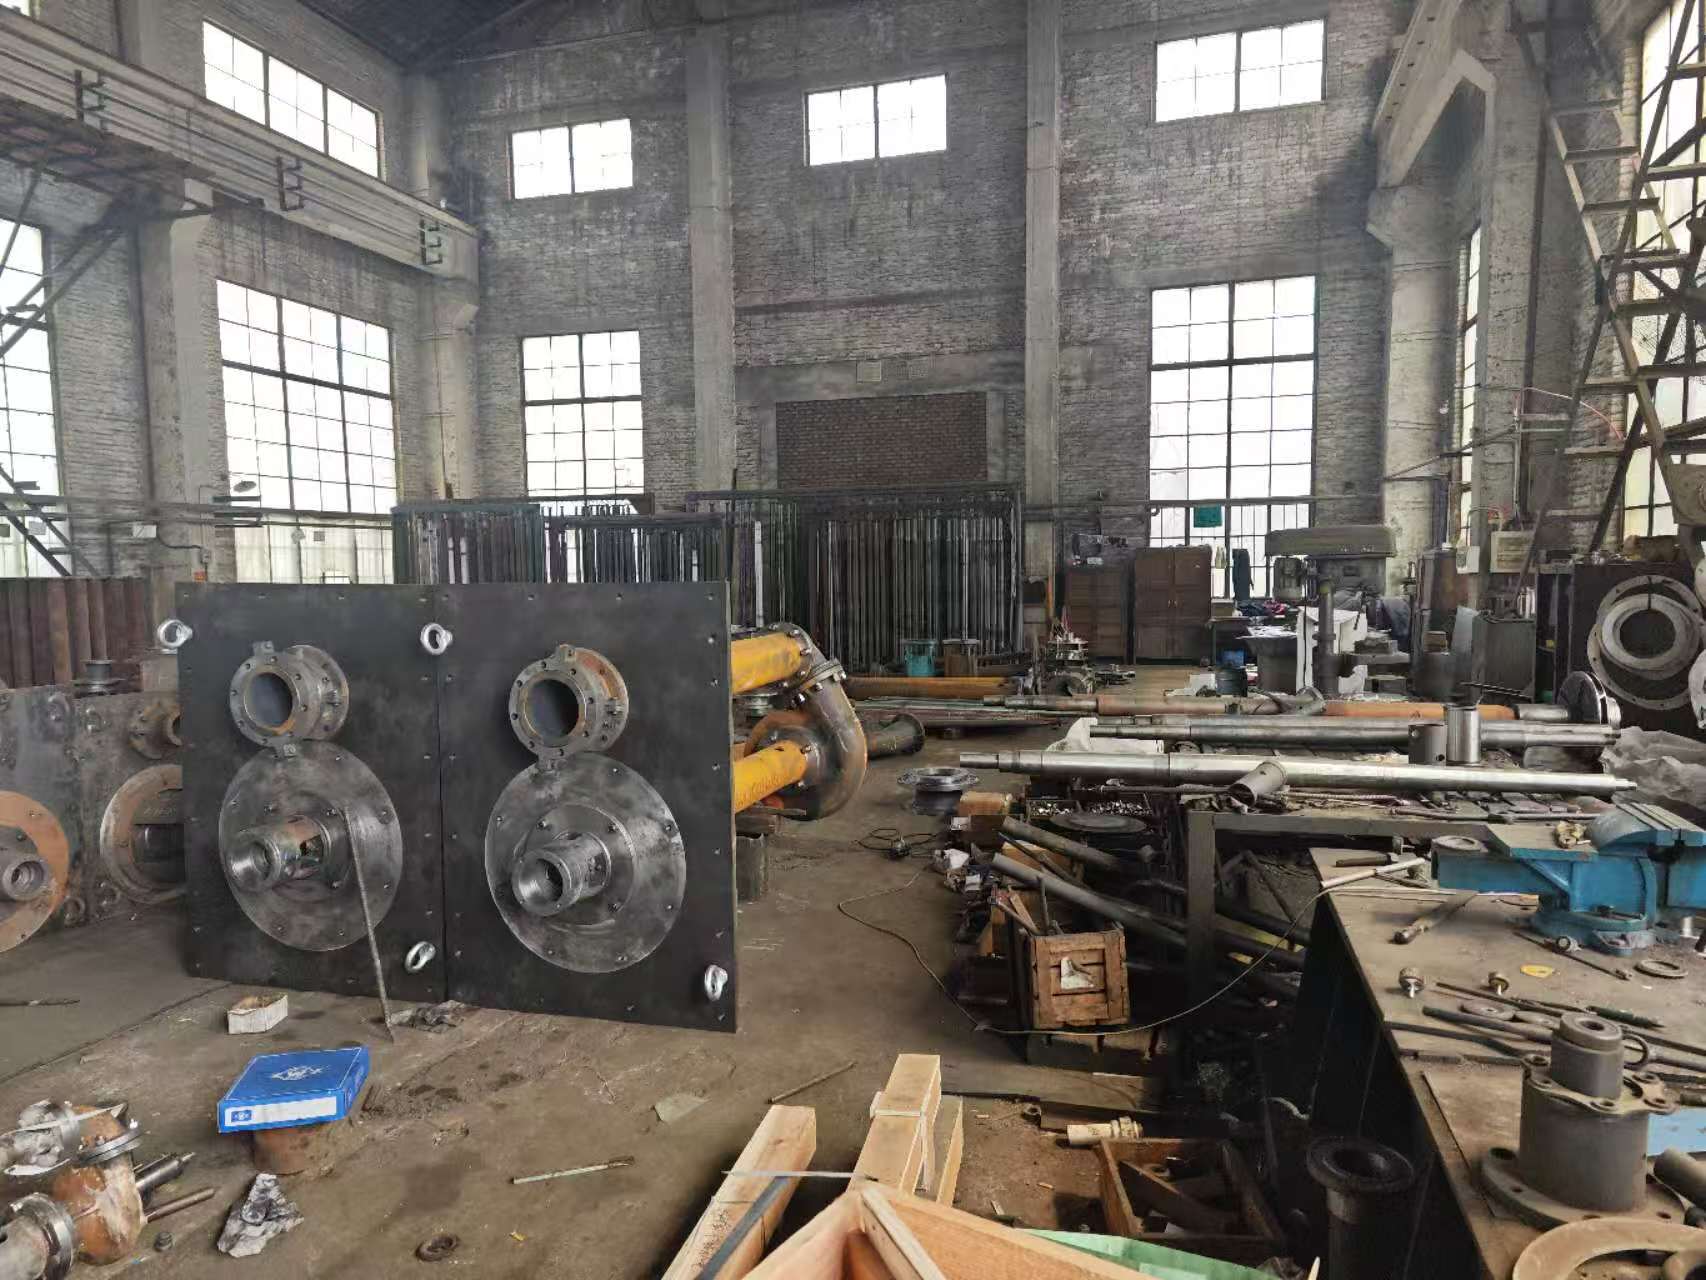
Manufacturing workshop 7
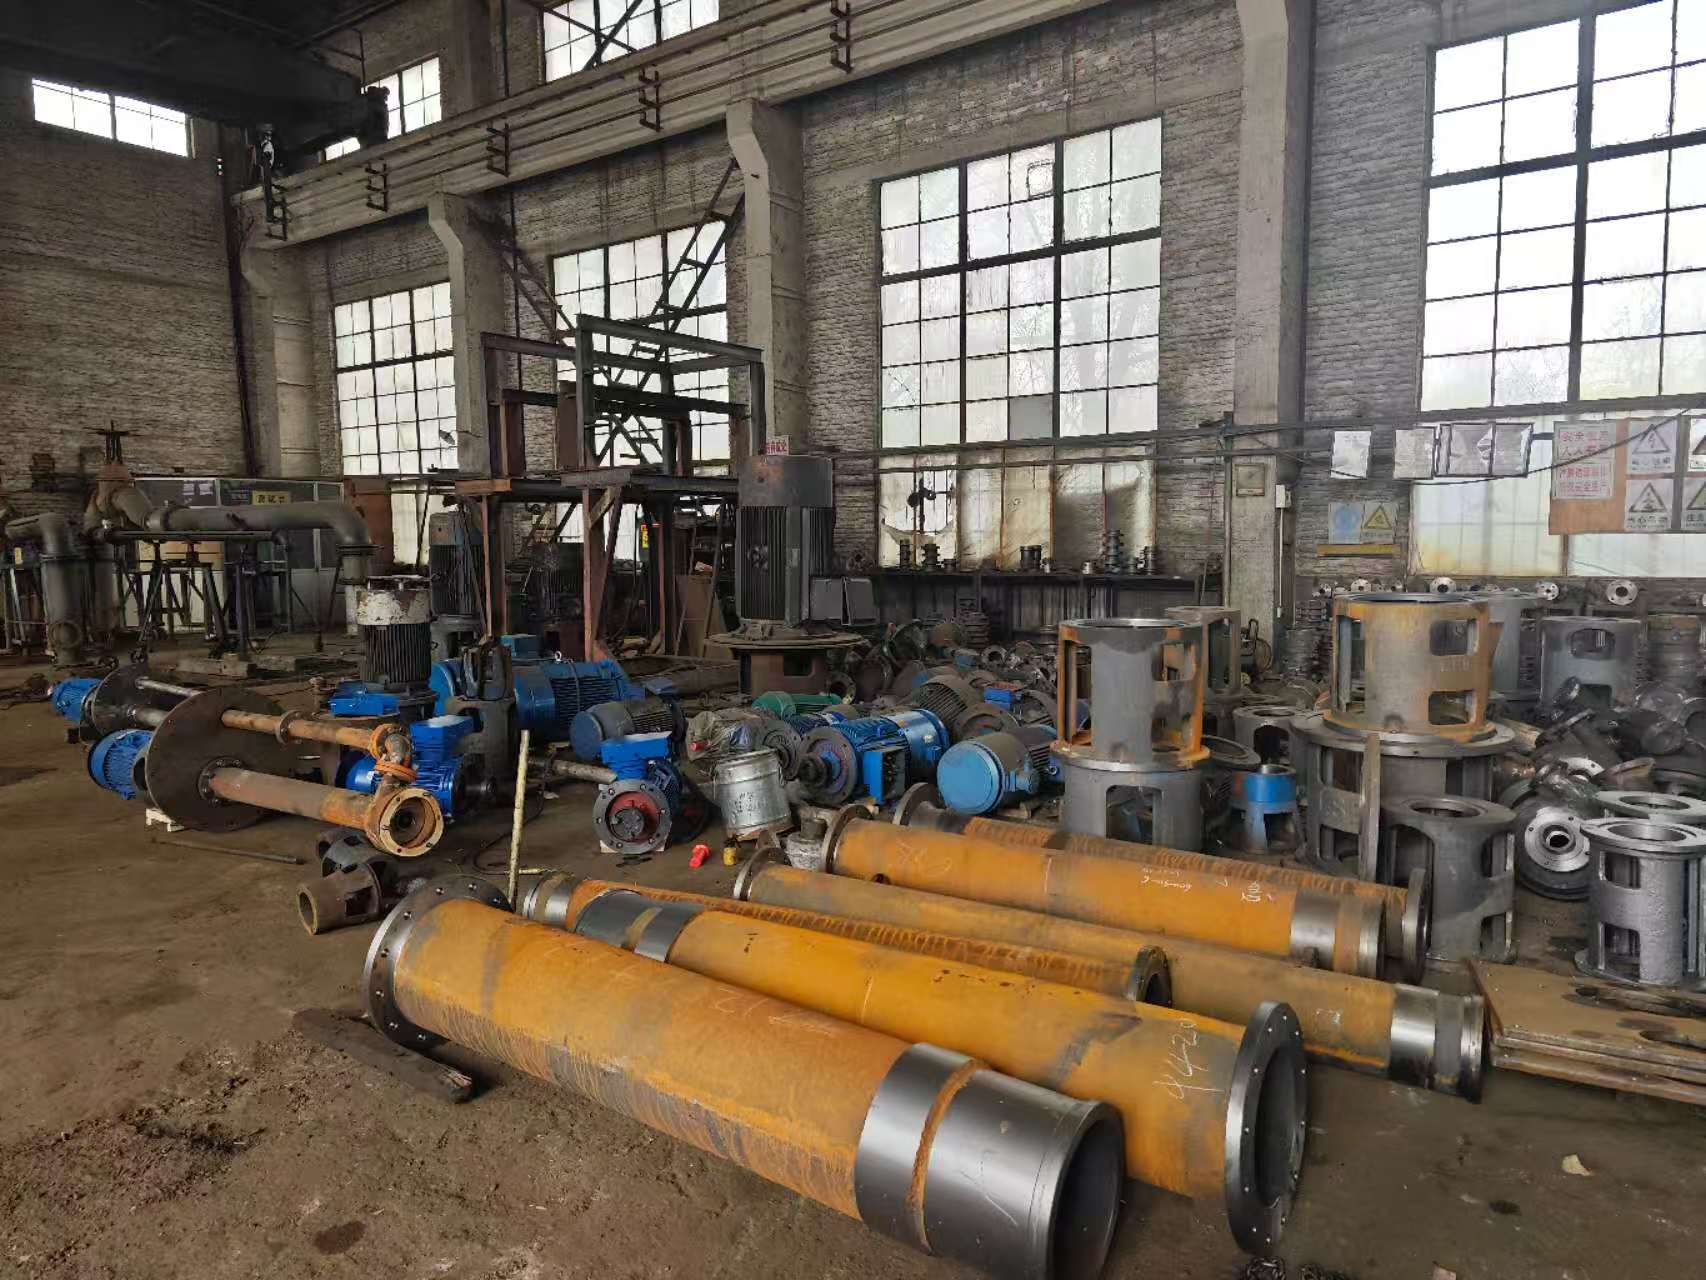
Manufacturing workshop 8
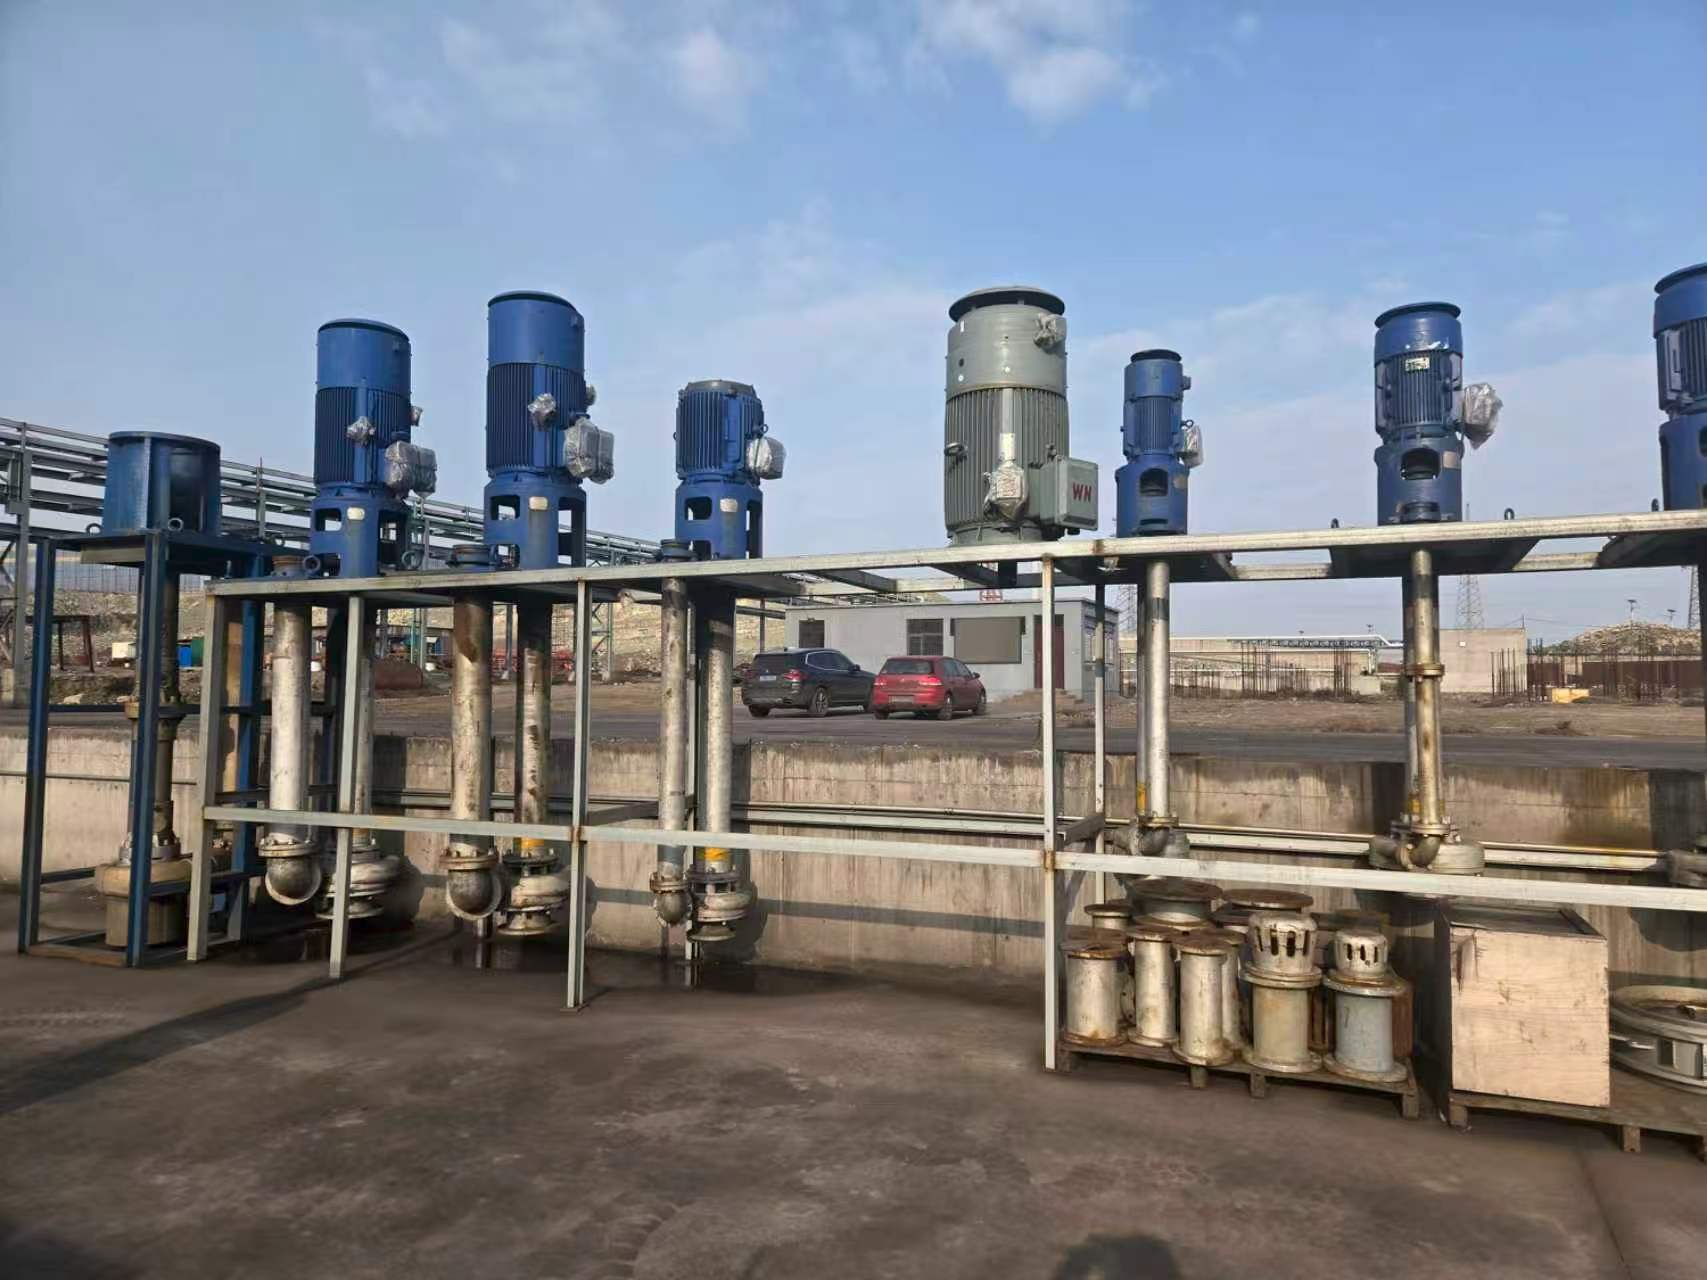
Manufacturing workshop 9
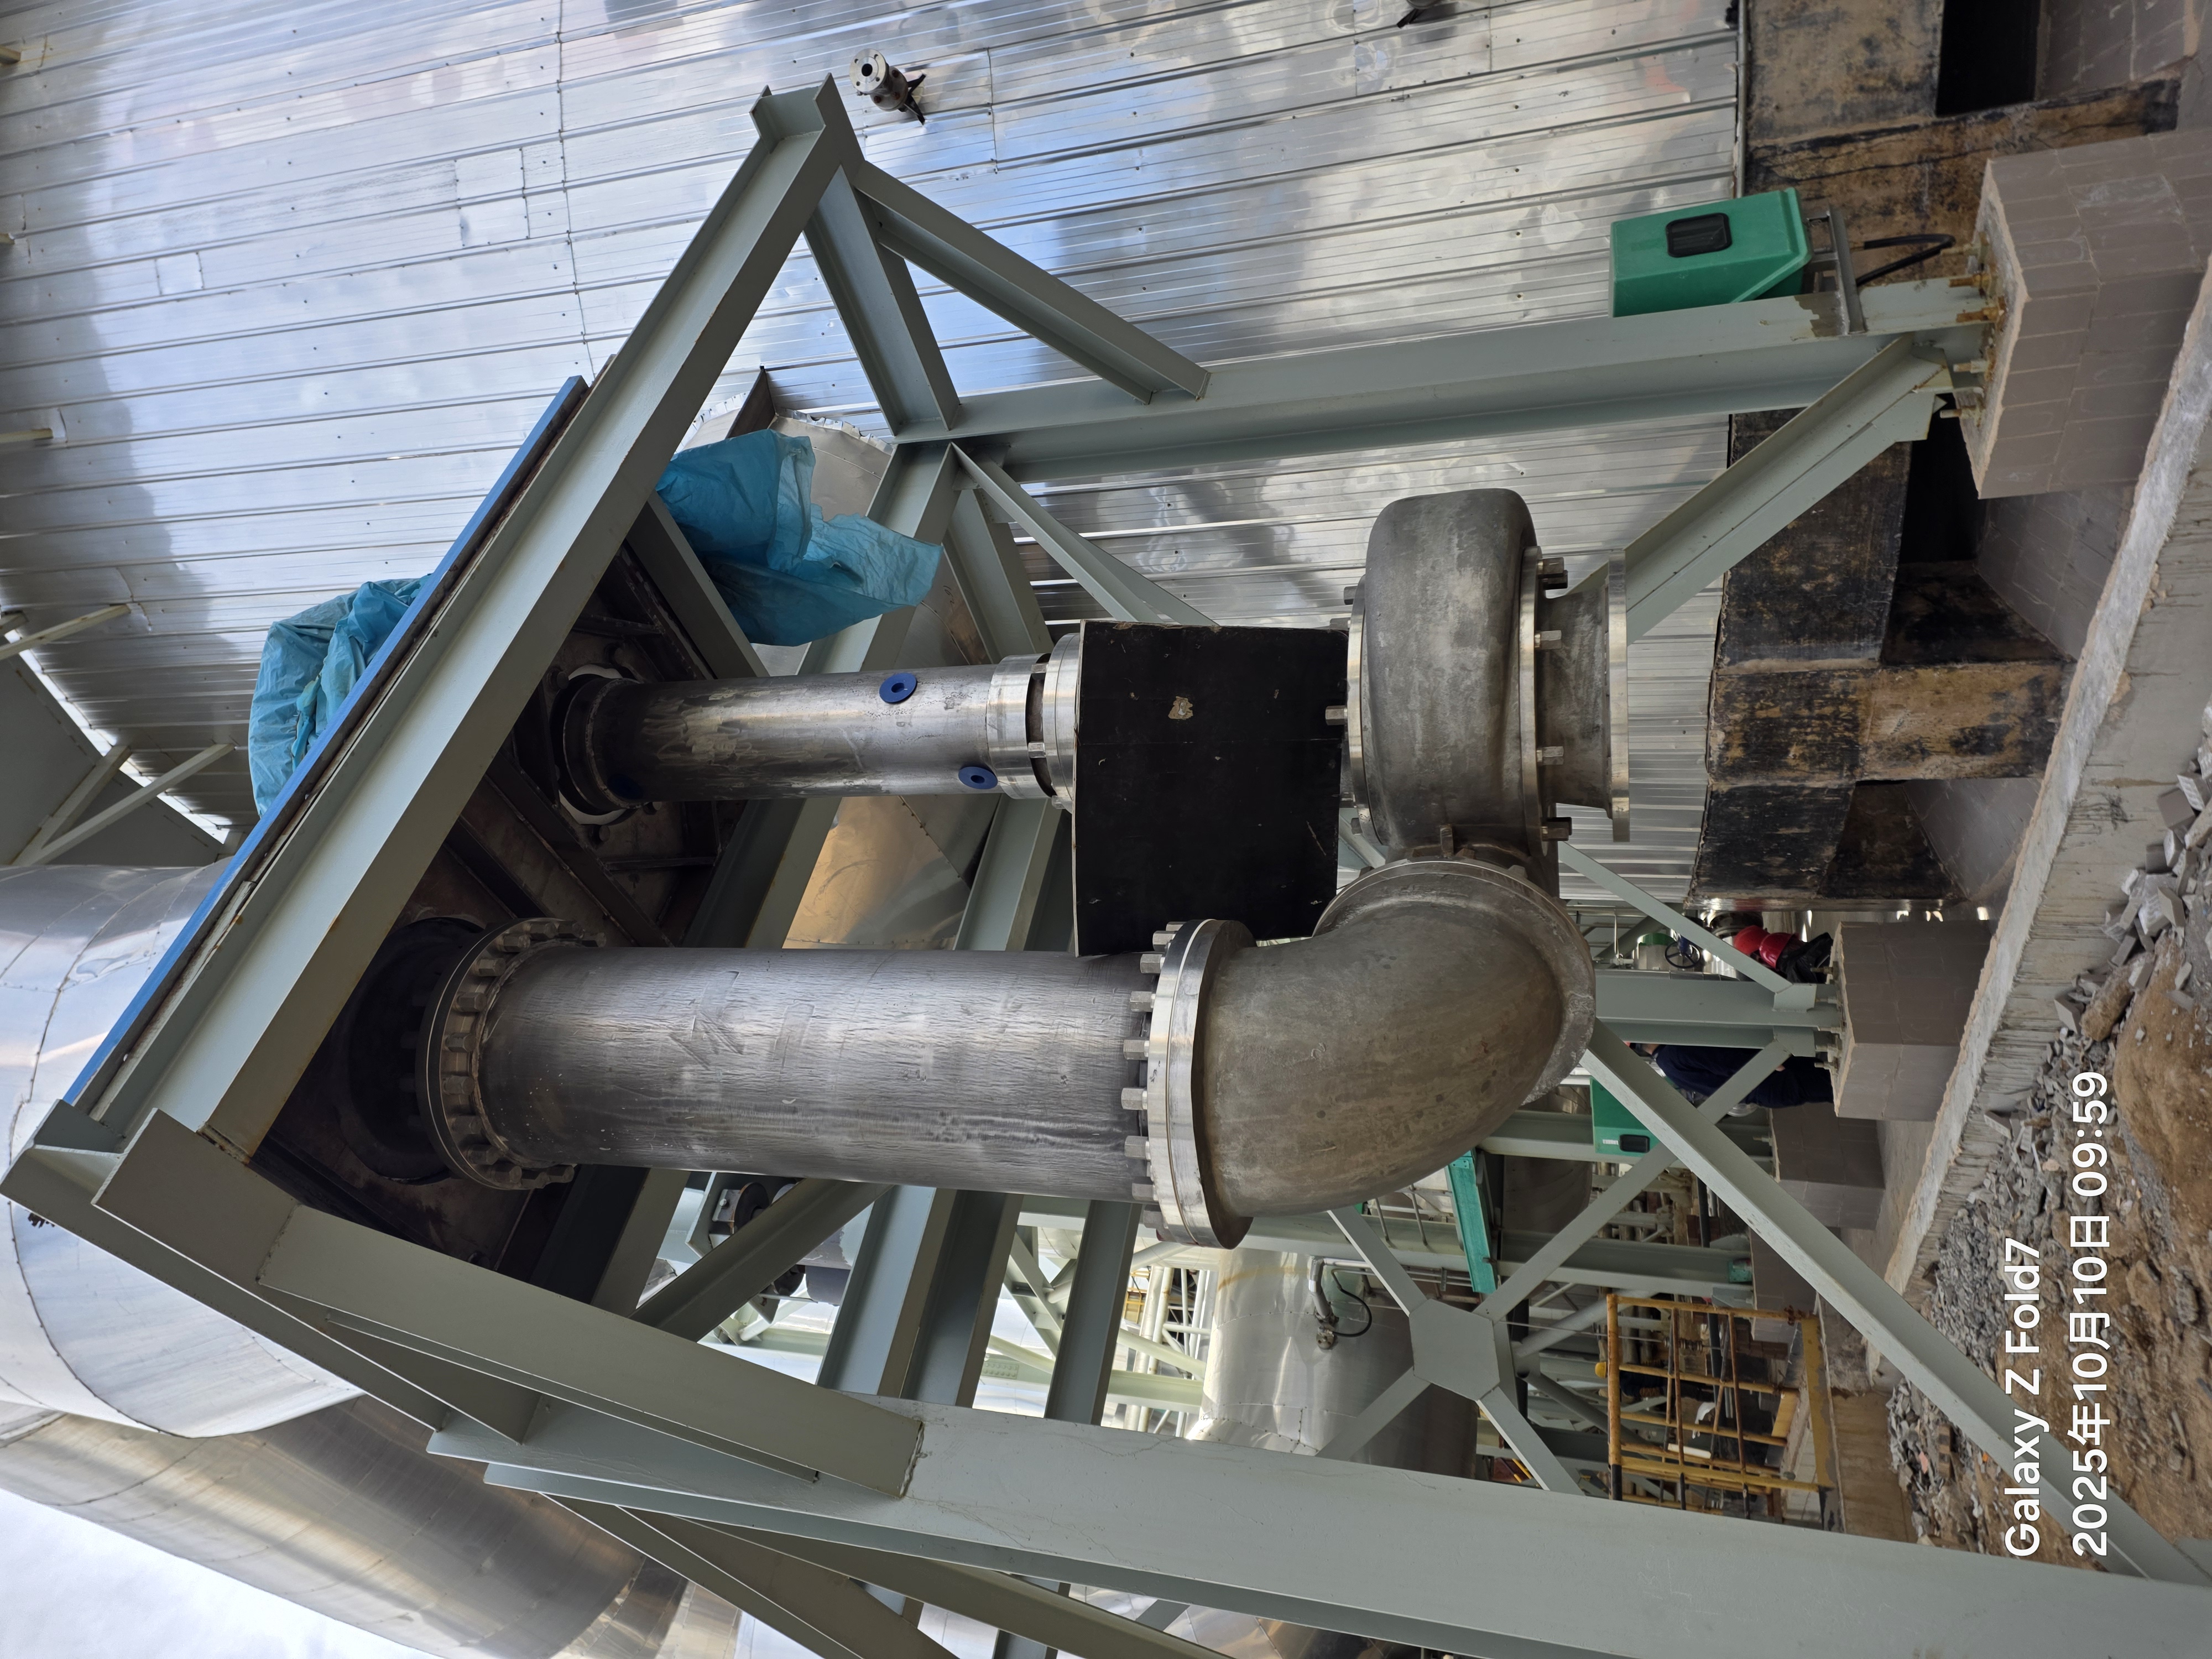
Manufacturing workshop 10
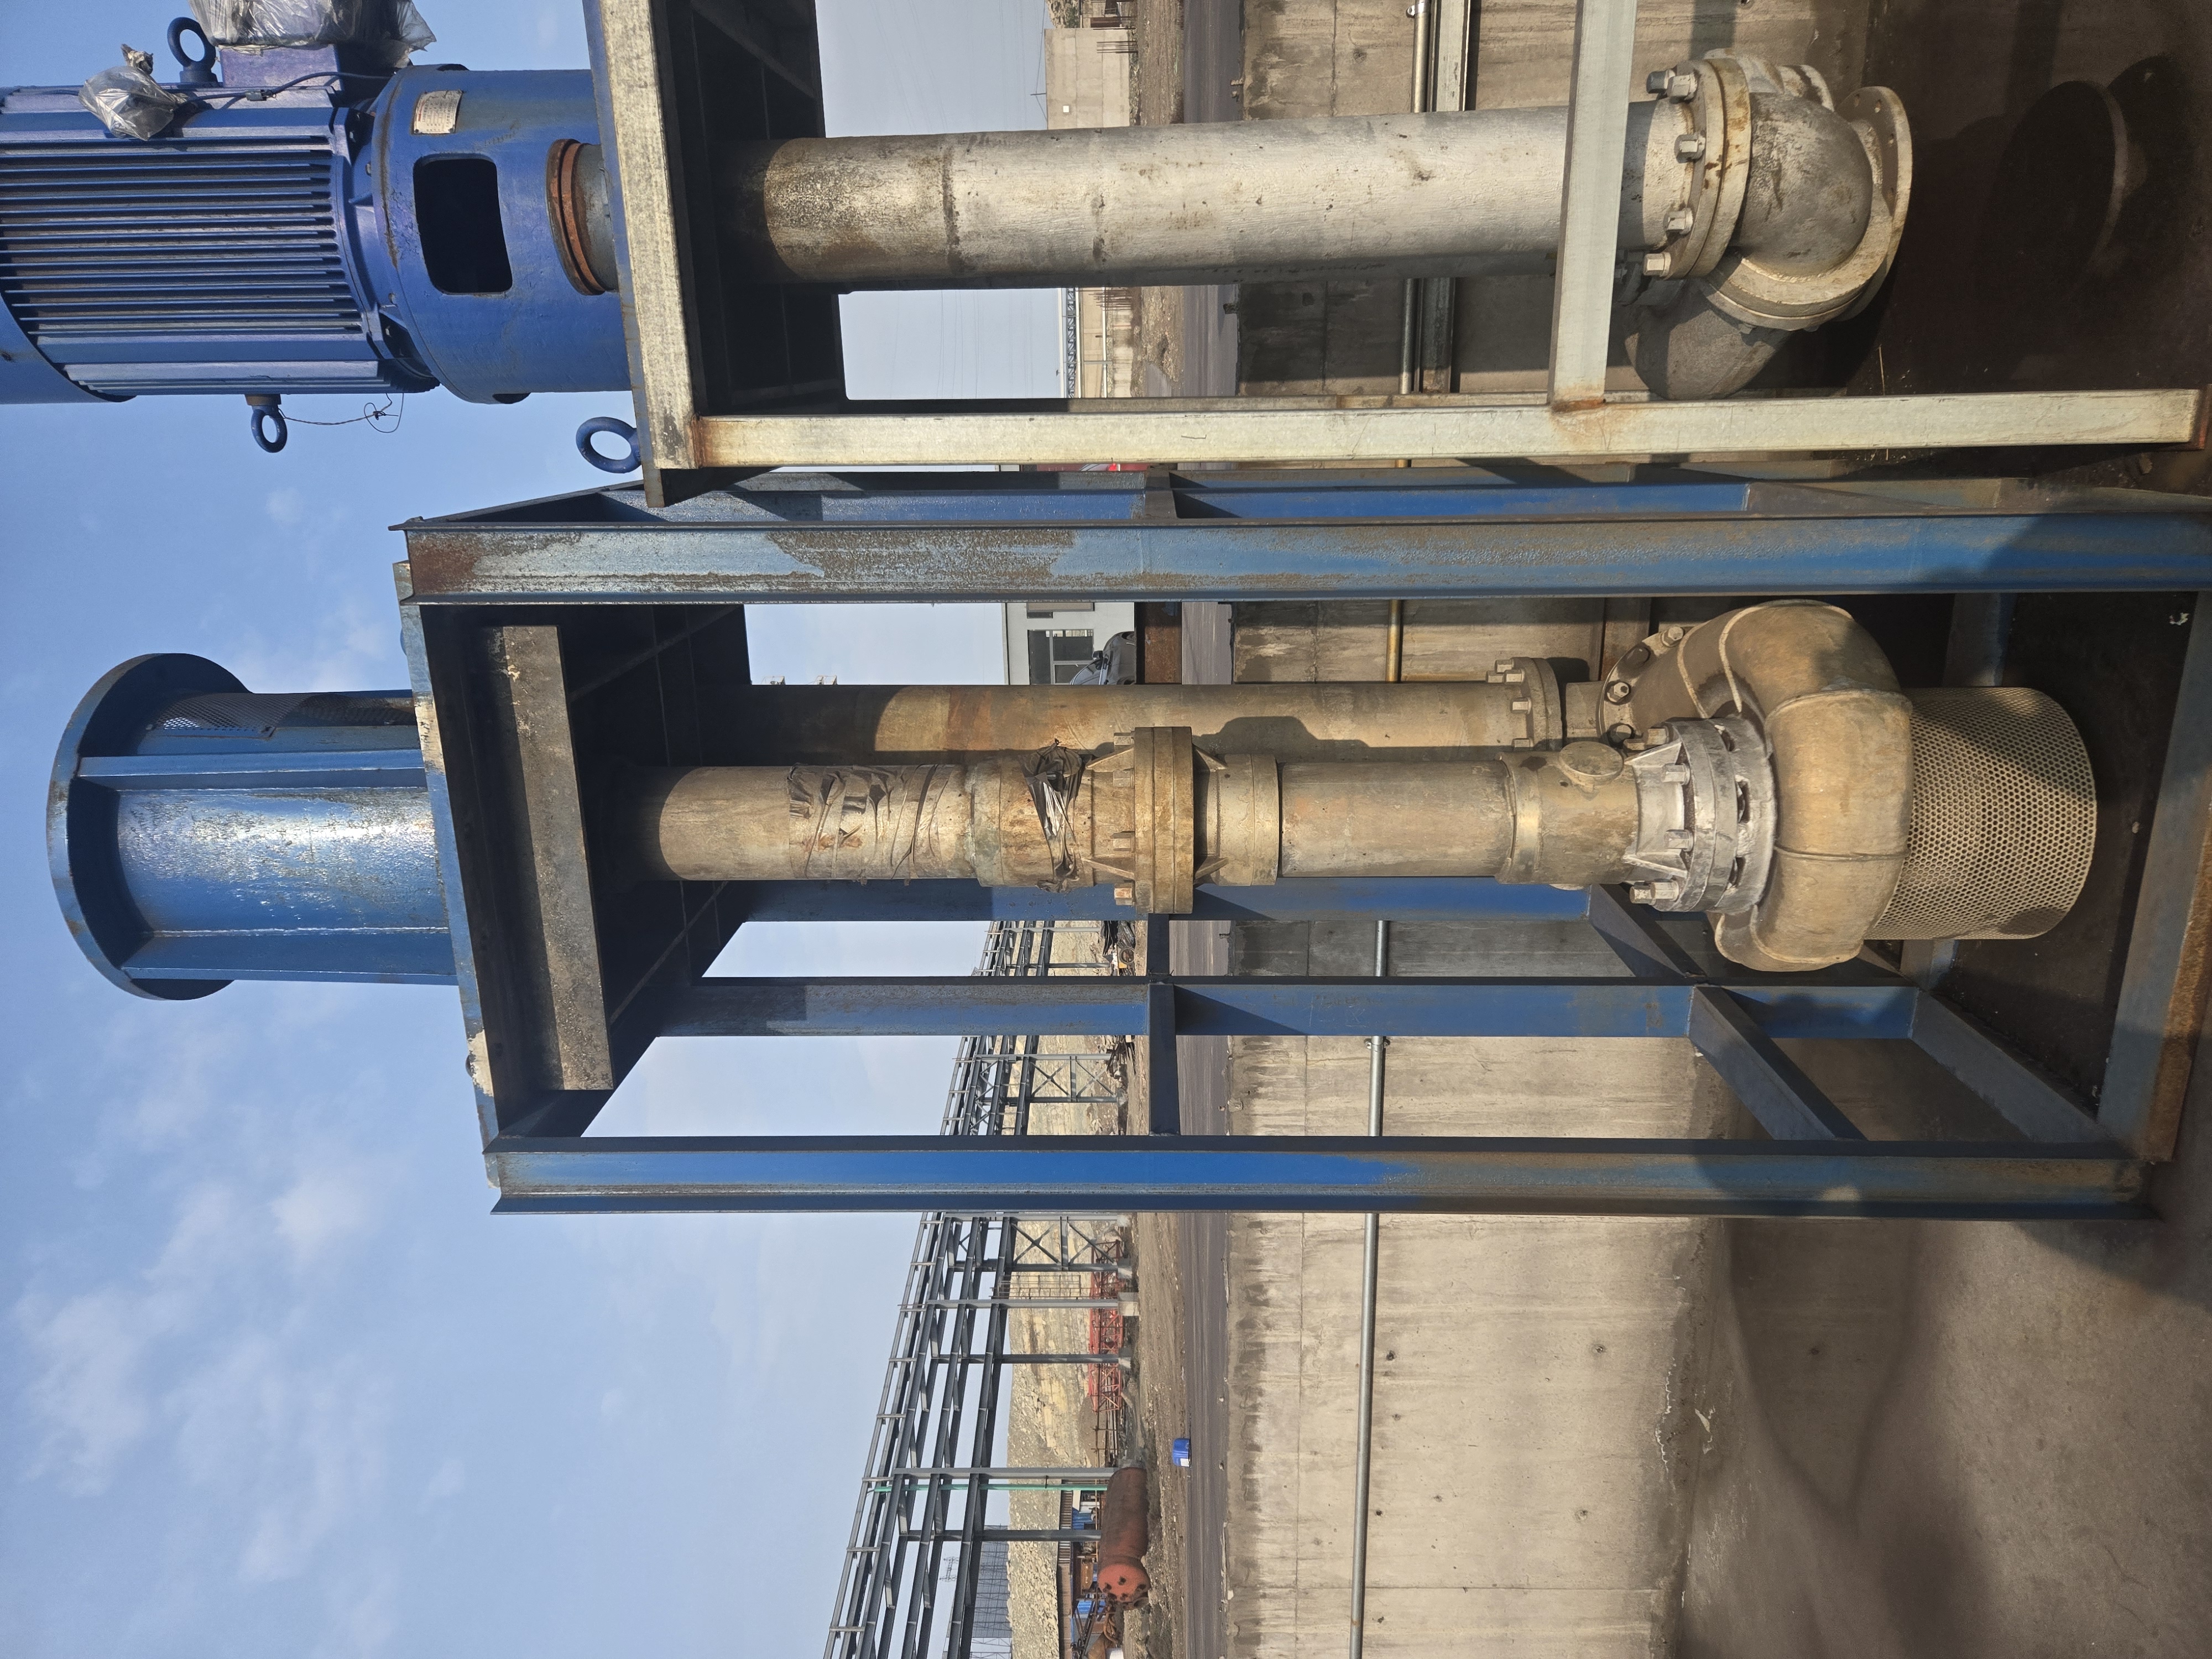
Manufacturing workshop 11
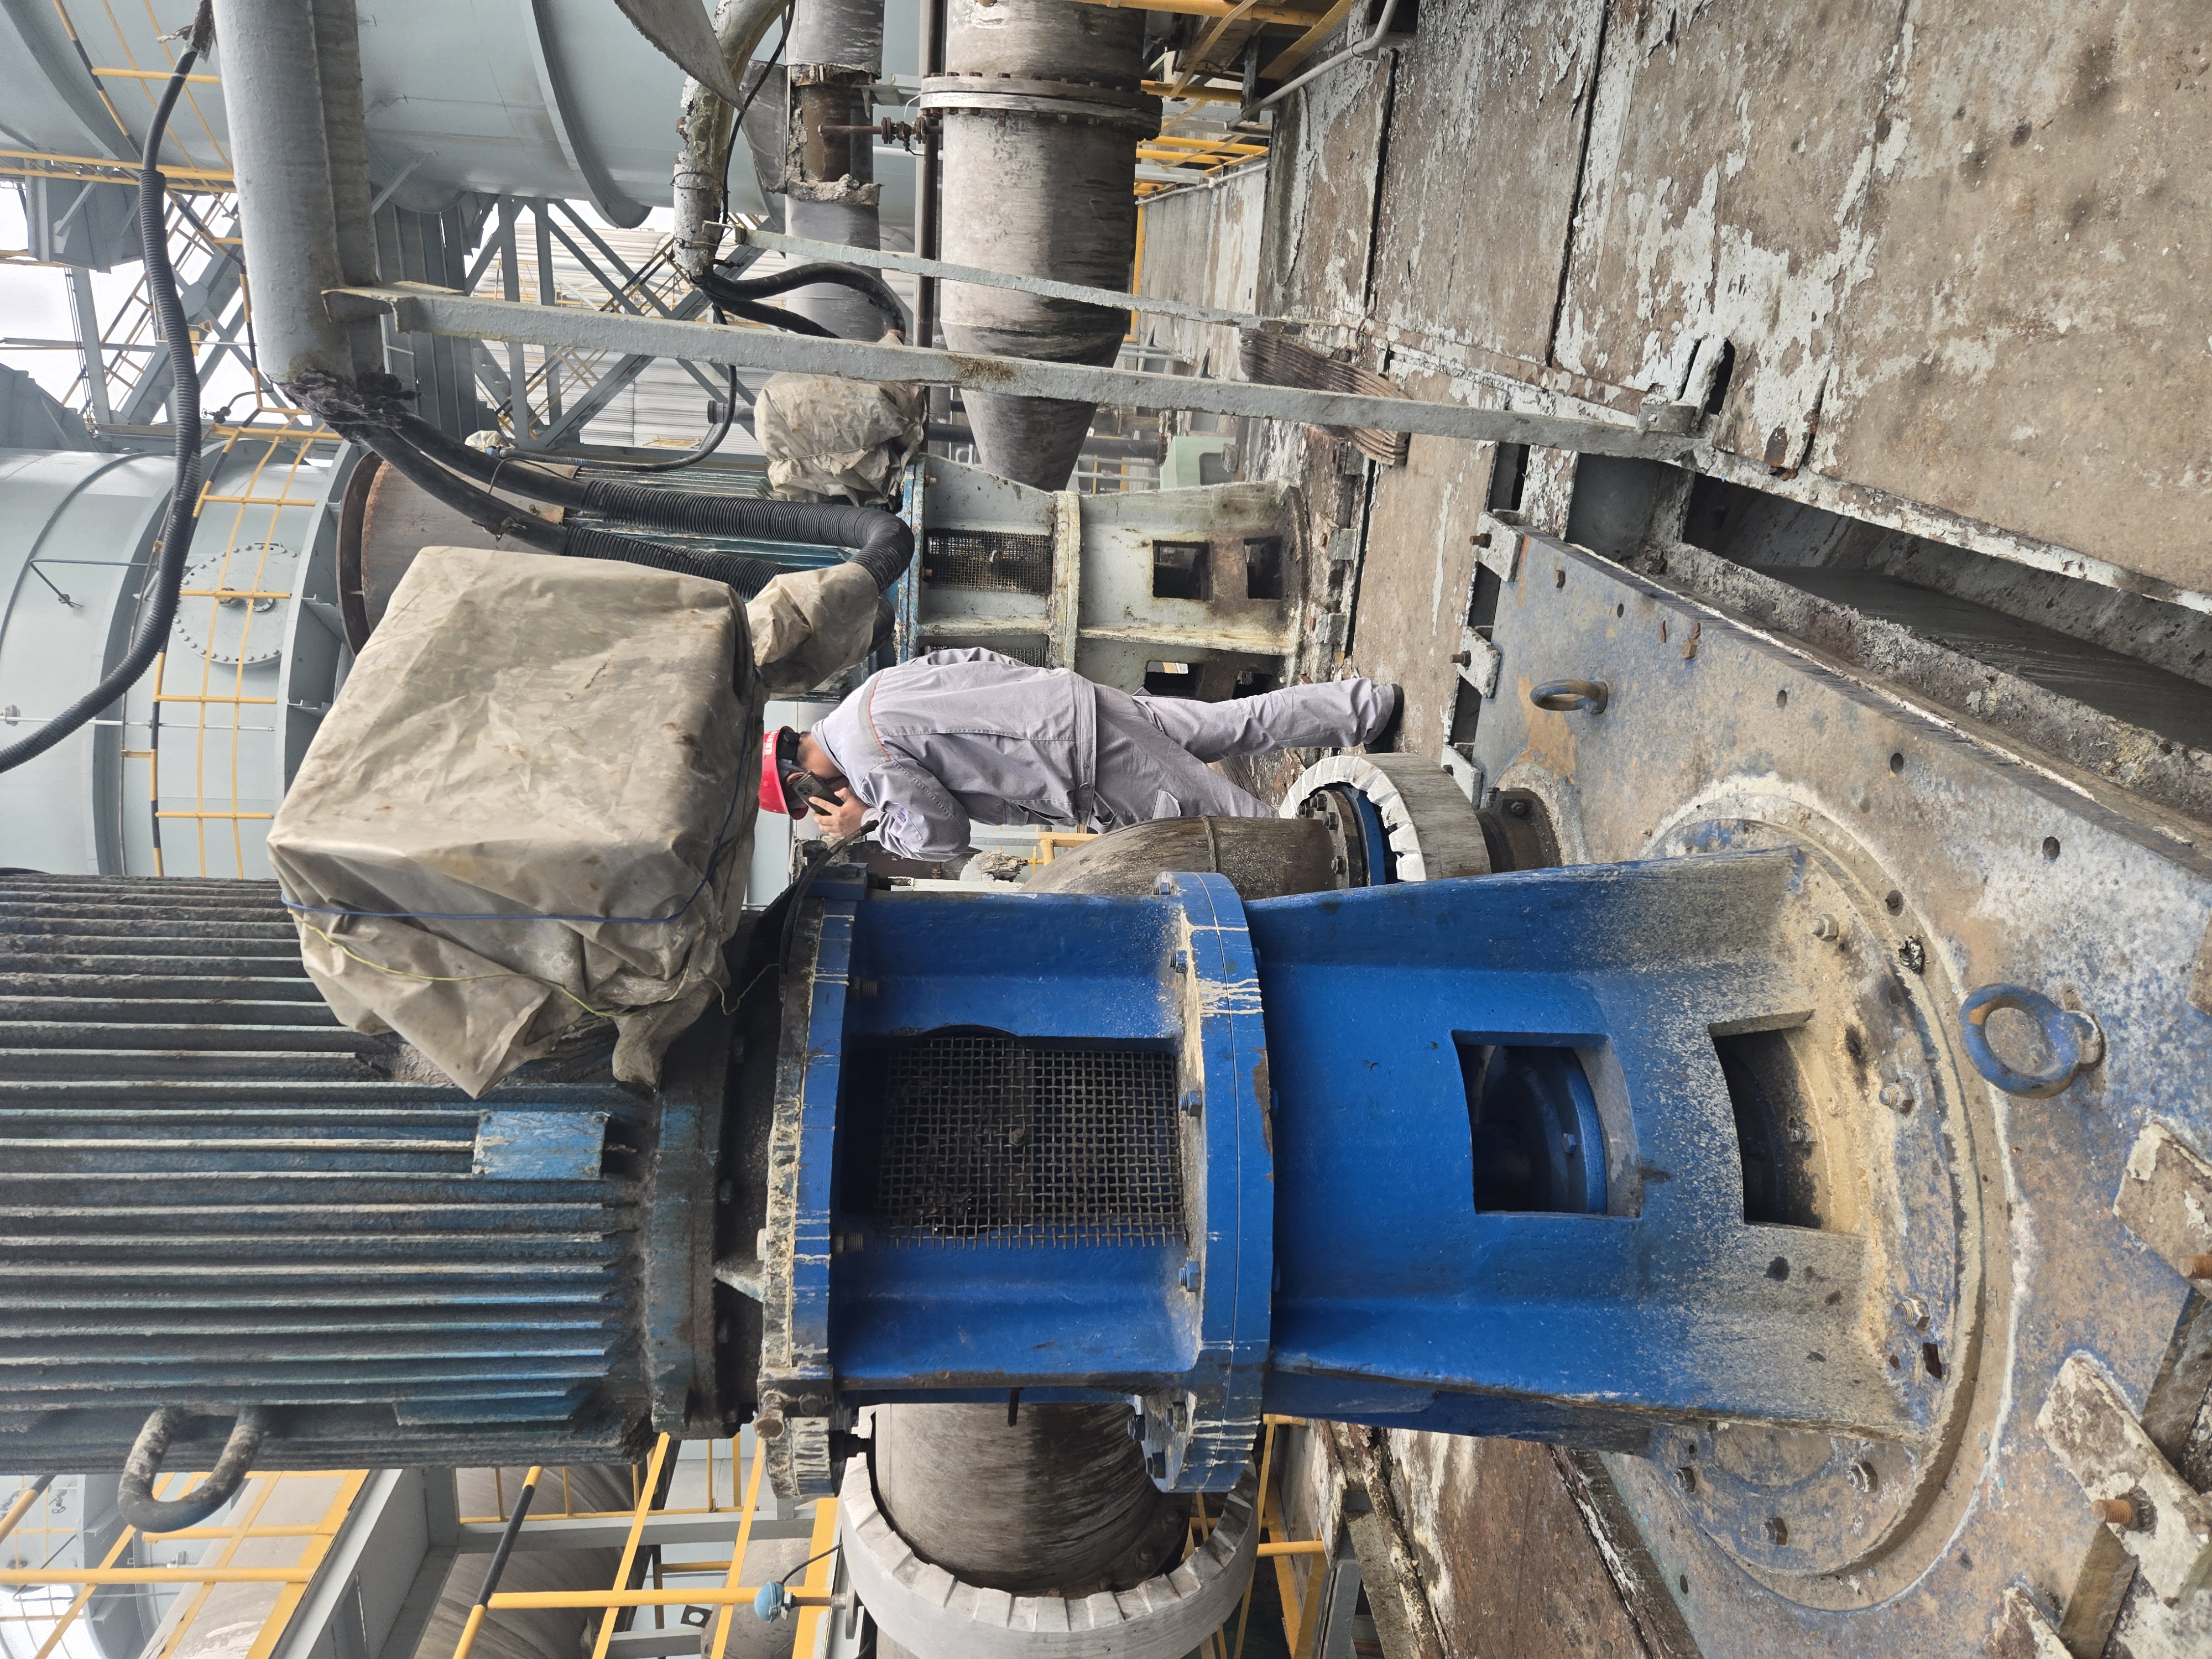
Manufacturing workshop 12
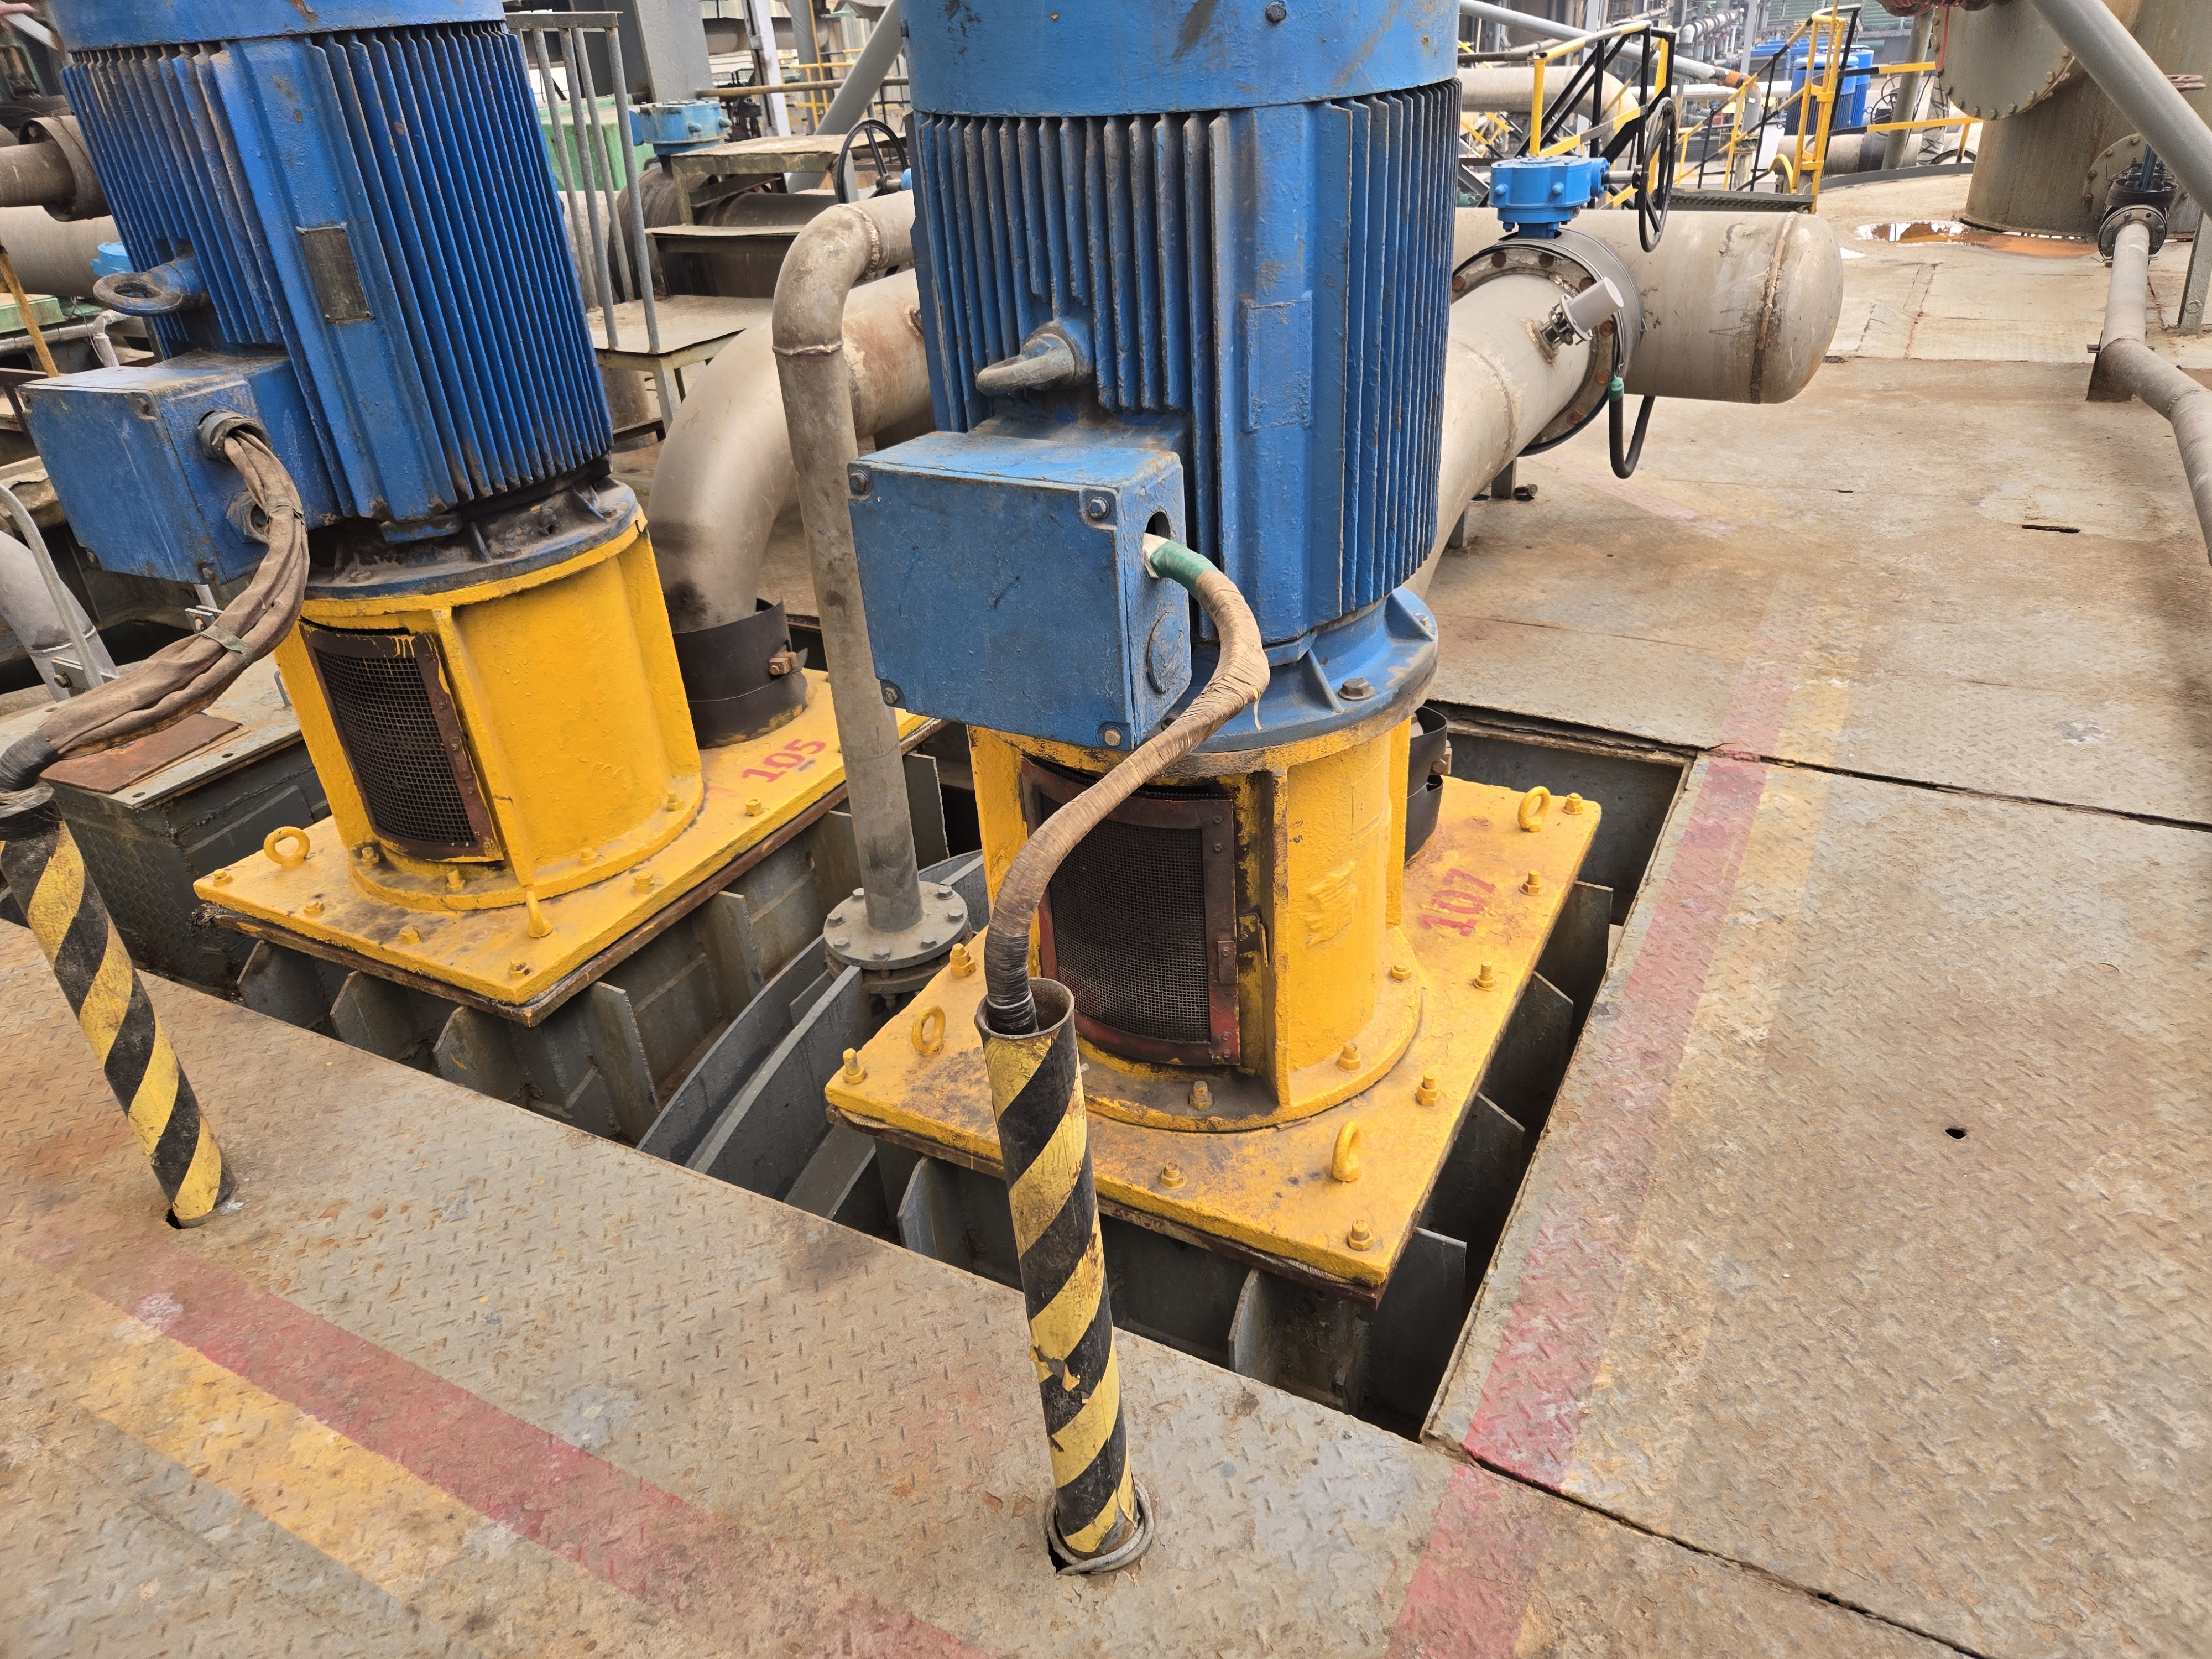
Manufacturing workshop 13
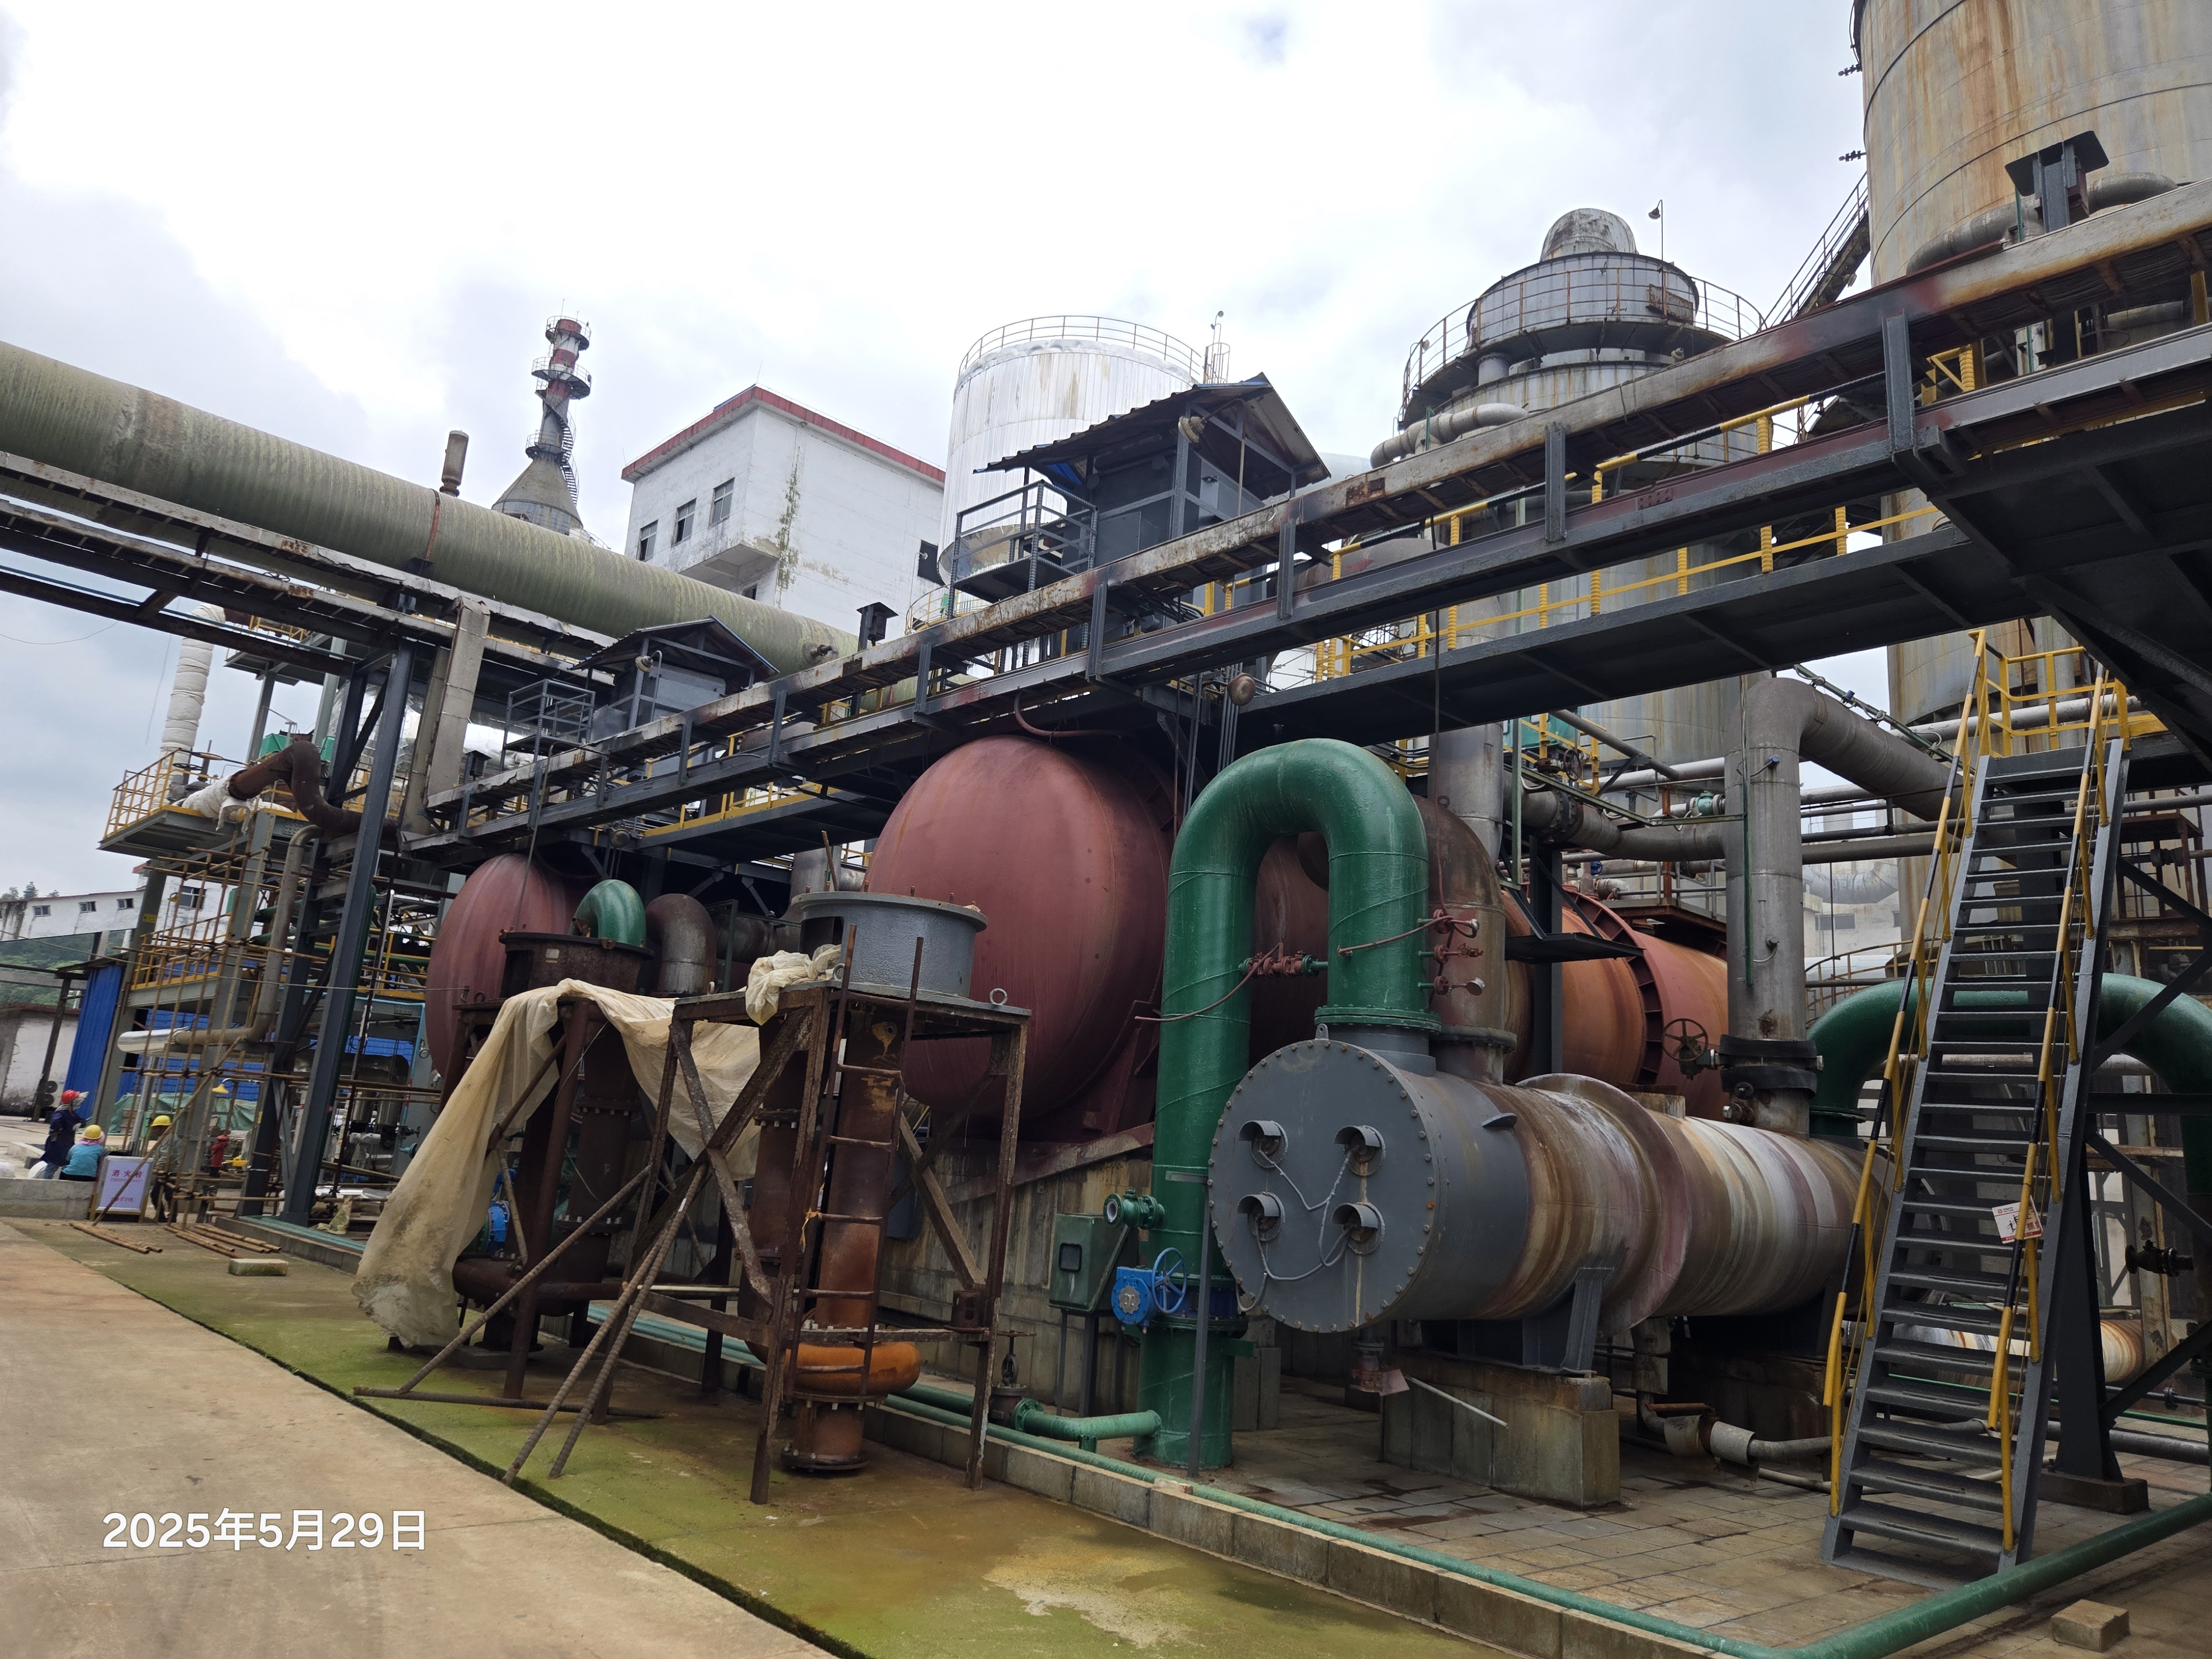
Manufacturing workshop 14
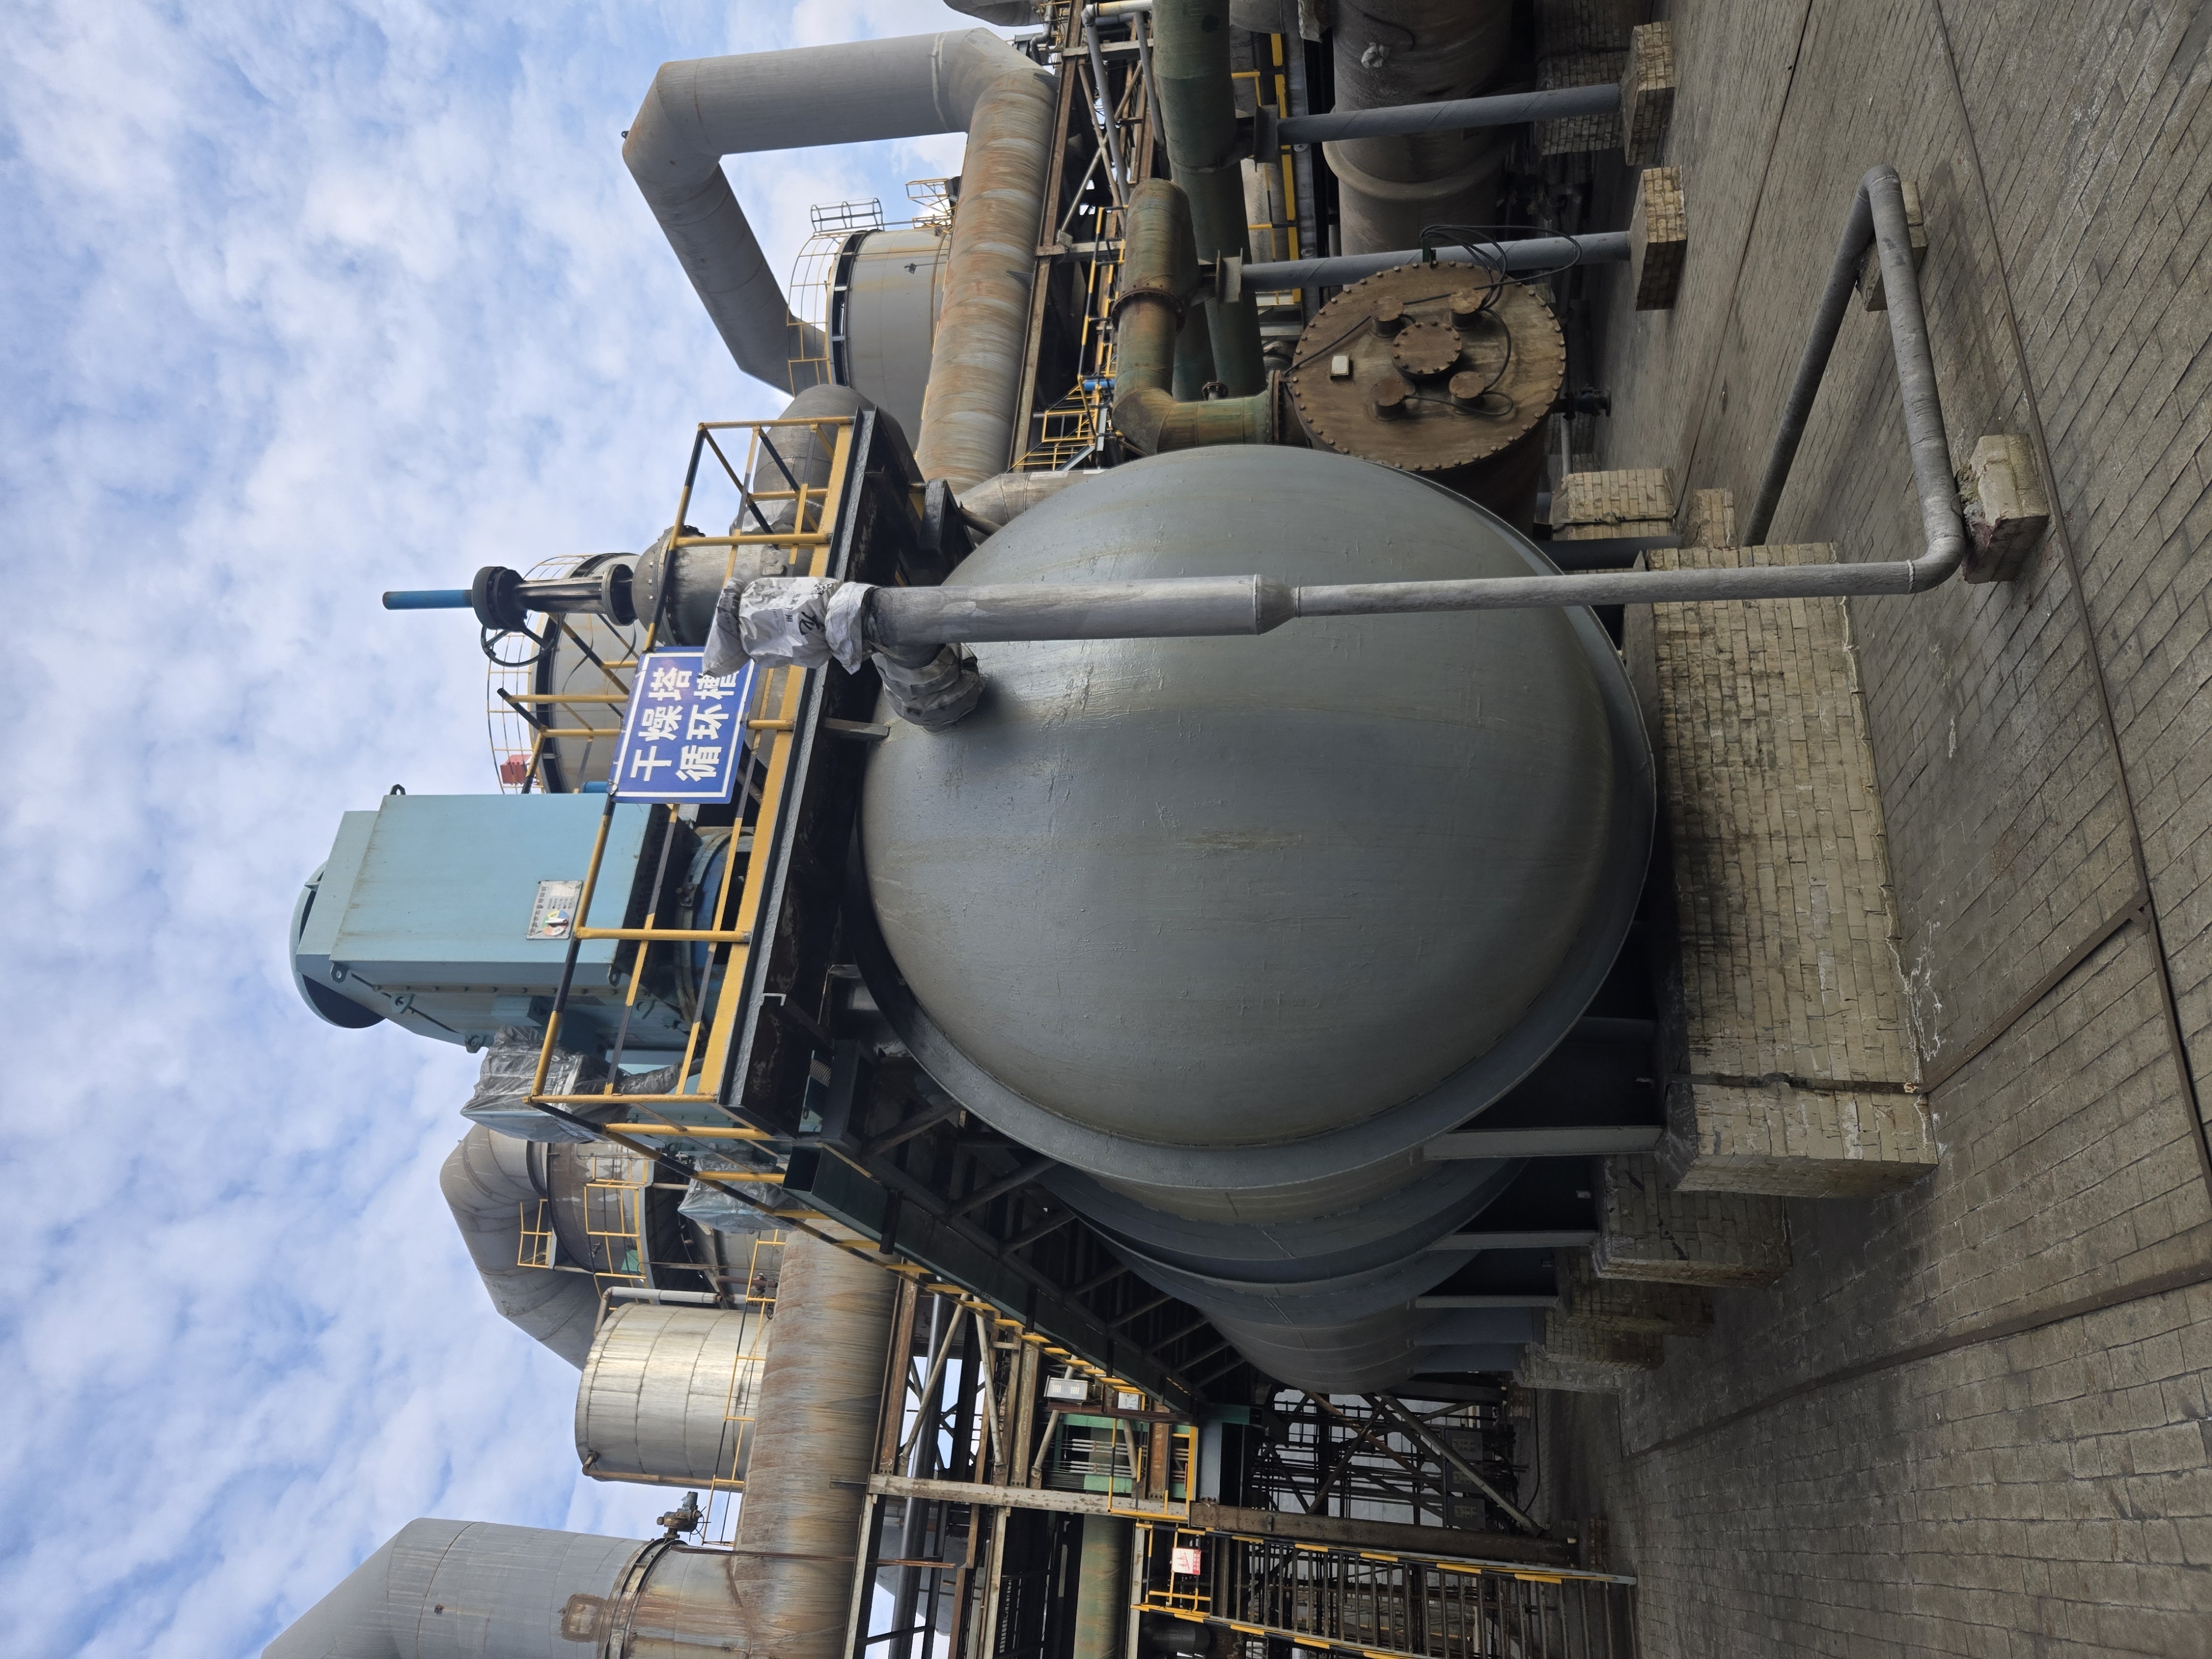
Manufacturing workshop 15
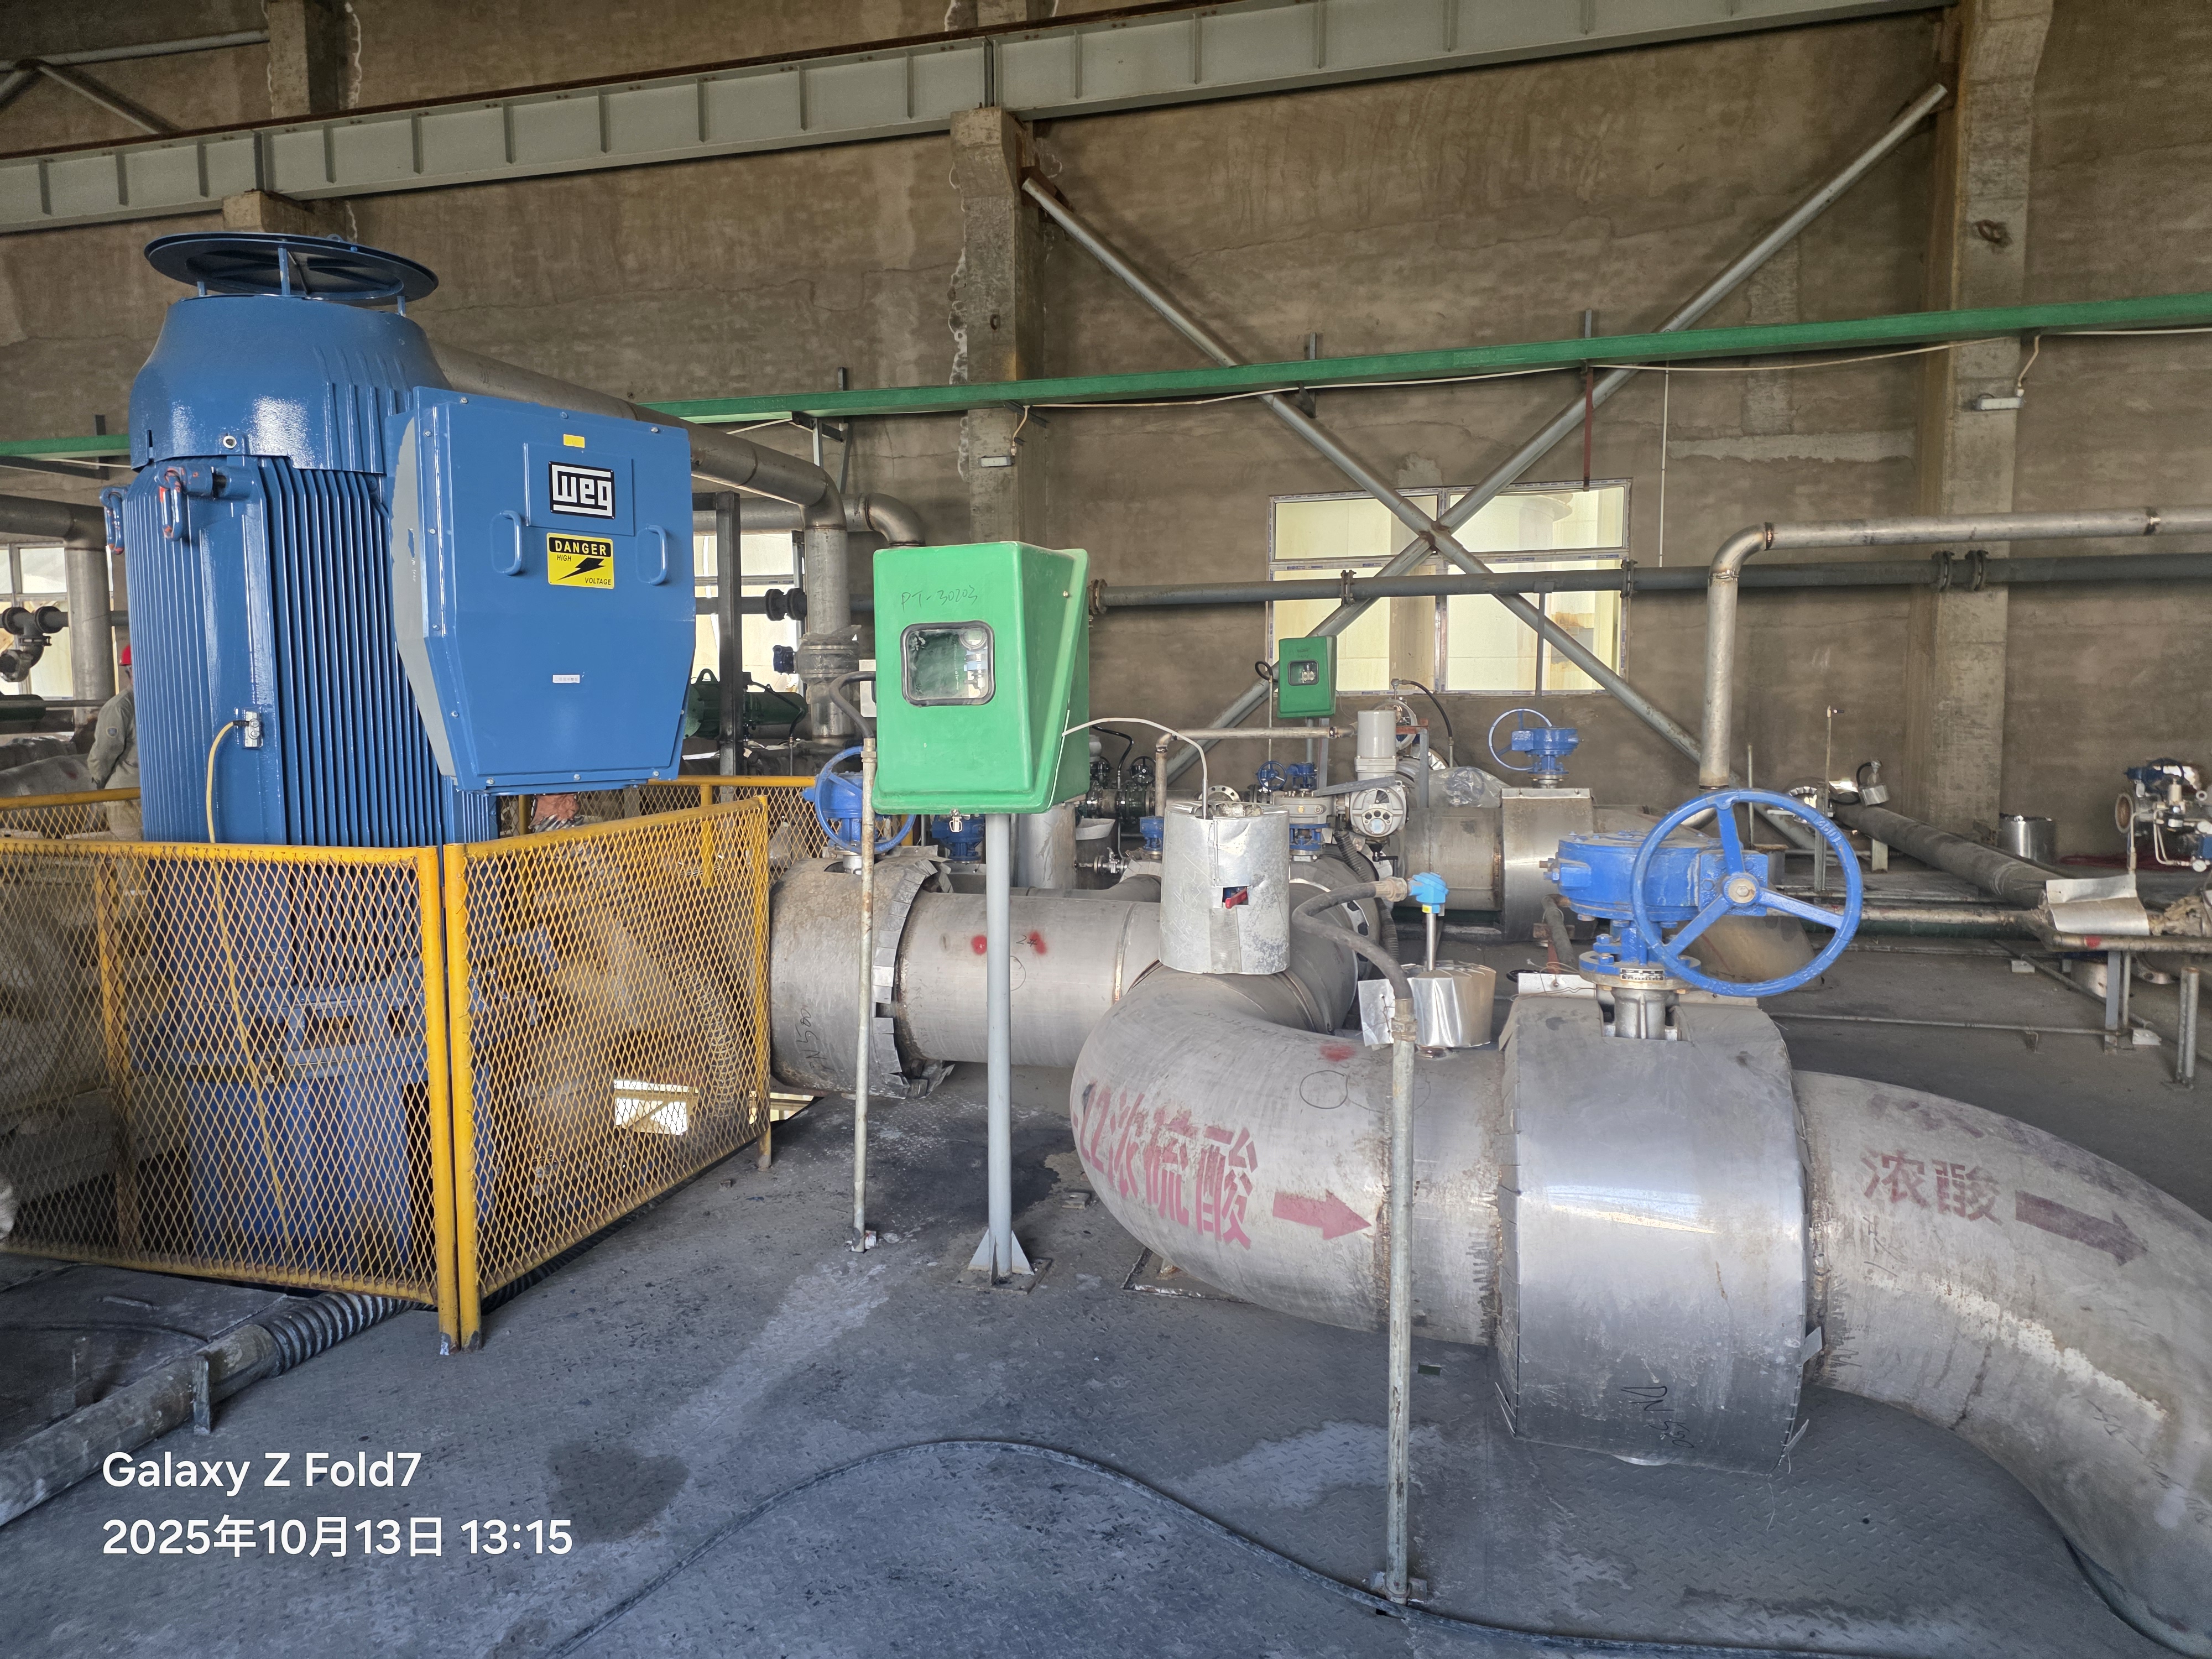
Manufacturing workshop 16
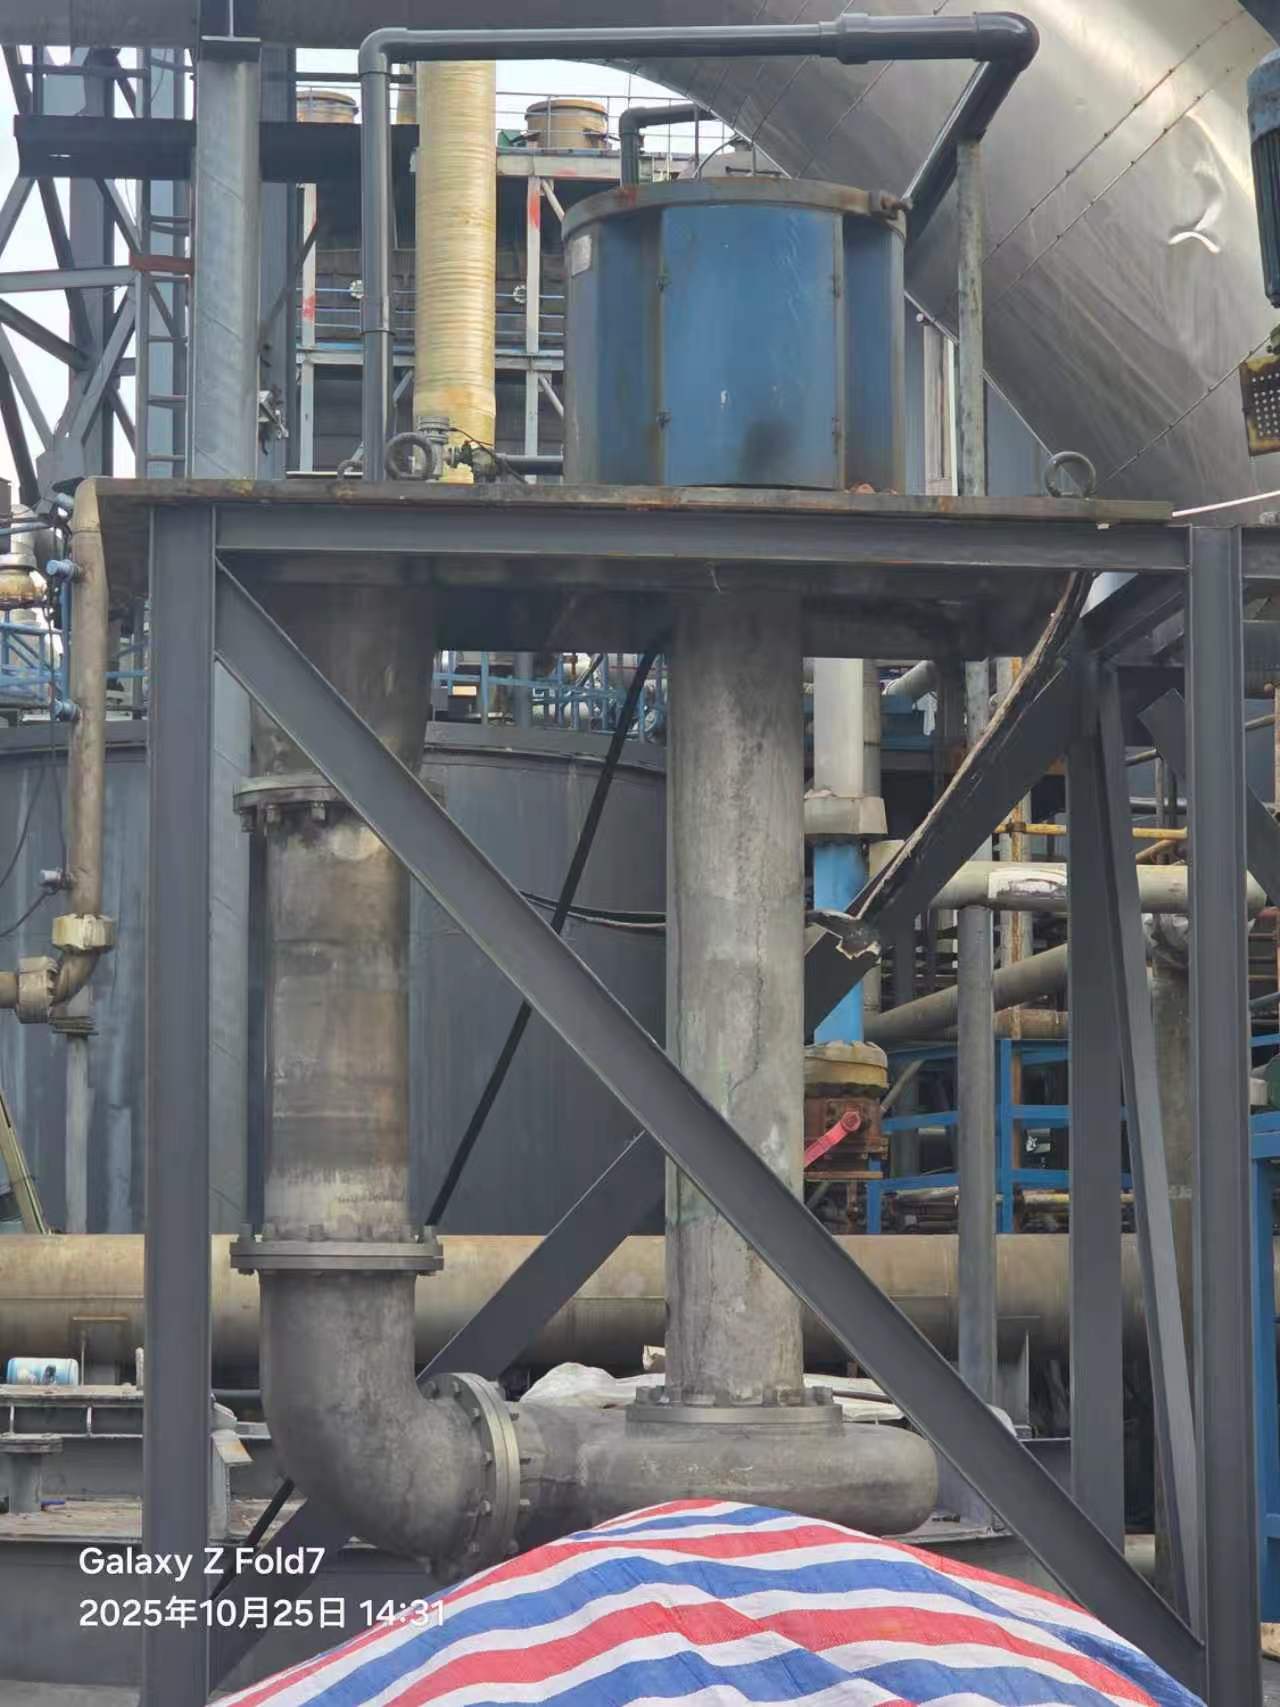
Manufacturing workshop 17